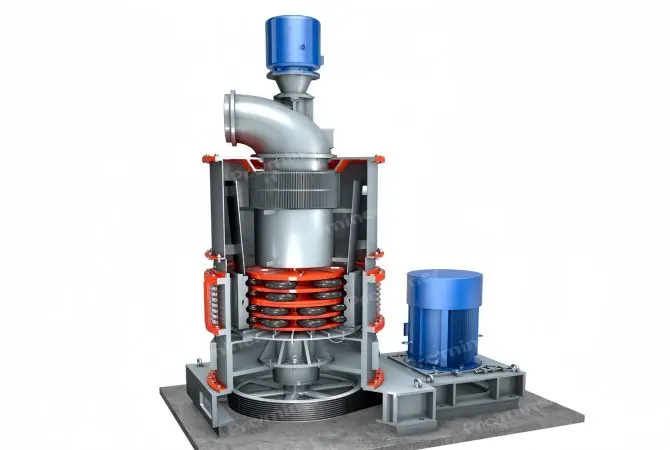
Flake graphite can be used to produce high carbon graphite, high purity graphite, expandable graphite

Molybdenum is an important industrial metal used in alloy steels, catalysts, lubricants, and chemical applications. The most common molybdenum mineral of economic value is molybdenite (MoS₂), which is typically recovered from ores by froth flotation. This process takes advantage of differences in the surface properties of minerals, allowing molybdenite to be separated from unwanted gangue minerals and, in many cases, from associated copper sulfides.
Molybdenum occurs in two main types of ore deposits:
Molybdenite has natural floatability because of its layered crystal structure and naturally hydrophobic surfaces. This characteristic makes flotation especially effective for its recovery. However, ore mineralogy, oxidation, fine particle size, and the presence of copper, iron sulfides, and clay gangue can complicate the process.
Flotation separates minerals by selectively attaching certain particles to air bubbles in a pulp of finely ground ore and water. In molybdenum flotation, the goal is to make molybdenite float while depressing other minerals.
The basic steps include:
Because molybdenite is naturally floatable, it often requires less collector than many other sulfide minerals.
Efficient recovery depends on liberating molybdenite from associated minerals without overgrinding. Molybdenite is soft and flaky, so excessive grinding can produce slimes, which float poorly and reduce concentrate quality.
Grinding is therefore carefully controlled to:
In many plants, staged grinding and classification are used to optimize recovery.
The flotation response of molybdenite is influenced by several reagents:
The exact reagent scheme depends heavily on ore type and whether molybdenum is being recovered as a primary product or separated from a bulk copper concentrate.
In porphyry copper-molybdenum ores, the usual practice is to first recover both copper sulfides and molybdenite together in a bulk concentrate. This is done because both mineral types are sulfides and can be floated under similar initial conditions.
The process generally involves:
This route is widely used because molybdenum commonly occurs at relatively low grades and is best concentrated along with copper before separation.
One of the most critical stages is the separation of molybdenite from chalcopyrite and other copper sulfides. This is usually accomplished by depressing copper minerals while allowing molybdenite to float.
Common methods include treatment with:
These reagents alter the surfaces of copper sulfides so they no longer attach readily to air bubbles, while molybdenite remains floatable. Multiple cleaning stages are often required to achieve a high-grade molybdenum concentrate.
The rougher flotation concentrate usually contains impurities, so it is upgraded through one or more stages of cleaning. Recleaning helps remove:
The number of cleaning stages depends on concentrate specifications. High-purity molybdenum concentrates require especially careful cleaning control, often combined with regrinding between stages.
Several factors can affect recovery and concentrate grade:
To overcome these problems, operators may adjust grind size, reagent dosages, pH, conditioning time, and flotation circuit design.
After flotation, the molybdenum concentrate is thickened, filtered, and dried. In some operations, further processing may be required to remove impurities or meet market specifications. The final concentrate is commonly marketed as molybdenite concentrate, which can then be roasted to produce molybdenum oxide or further refined into other molybdenum products.
Successful molybdenum recovery by flotation depends on close control of:
Modern plants often use automated monitoring and sampling systems to maintain recovery and product quality.
Molybdenum ores are recovered by flotation mainly because molybdenite possesses natural hydrophobicity, making it highly amenable to this method. The process usually involves crushing, controlled grinding, reagent conditioning, rougher flotation, and multiple cleaning stages. In copper-molybdenum ores, bulk flotation is followed by selective separation, where copper sulfides are depressed and molybdenite is floated. With proper control of liberation, reagents, and circuit conditions, flotation can produce high recoveries and high-grade molybdenum concentrates for downstream processing.
A: A handful of variables drive most of the variation in recovery and grade: grind size (liberation), pulp density, reagent type and dosage, residence time, pH, and — for magnetic separation — field intensity and feed rate. Changing one without adjusting the others usually backfires. The practical way to find your optimum is a structured test program: vary one parameter at a time on your actual ore and measure recovery and grade at each point. We run this kind of parameter study during lab and pilot testing, then carry the settings into the plant design and re-tune them during commissioning.
A: Three properties matter most: whether the valuable mineral is sulfide or oxide, how coarsely or finely it is disseminated in the gangue, and what gangue minerals accompany it. Coarse, high-density minerals respond well to gravity separation; magnetic minerals to magnetic separation; fine sulfide minerals to flotation; oxide or low-grade ores often to leaching. Many ores need a staged combination. Because two deposits carrying the same metal can behave completely differently, the flowsheet has to be built from your ore’s own test data — not copied from a similar project.
A: A single method rarely hits both target recovery and target grade when the ore contains multiple valuable minerals, spans a wide particle size range, or carries problematic gangue. Then a combined flowsheet is justified — for example, gravity pre-concentration to reject coarse waste early, magnetic separation ahead of flotation to remove magnetic minerals, or staged grinding and classification to liberate progressively. The added circuit costs more, but it usually pays back through higher overall recovery and lower reagent and energy consumption per tonne.
A: Refractory ores resist standard processing — gold locked inside sulfide minerals, ores that consume excessive reagents, carbonaceous ores that re-adsorb dissolved gold, fine or clay-rich ores that slime badly, or oxide ores that float poorly. Treatment usually adds a step ahead of or instead of the conventional circuit: finer grinding, oxidation pre-treatment, roasting, or a switch from flotation to leaching. Identifying the specific cause through diagnostic testwork is essential, because each cause has a different fix and the wrong one wastes capital.
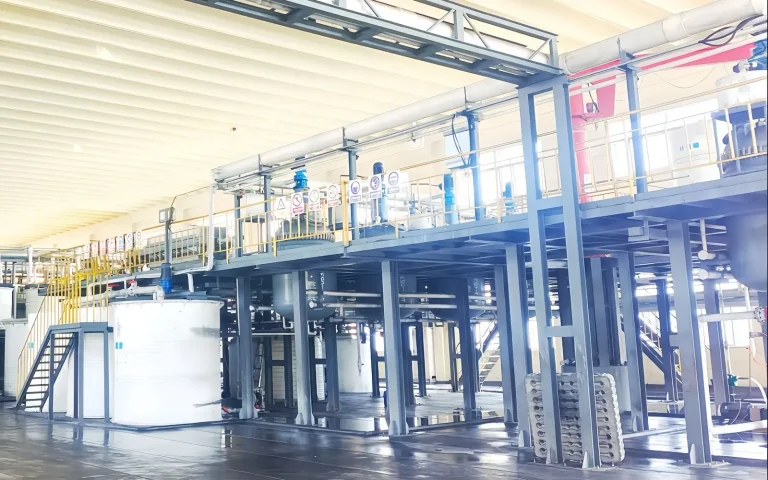
Flake graphite can be used to produce high carbon graphite, high purity graphite, expandable graphite
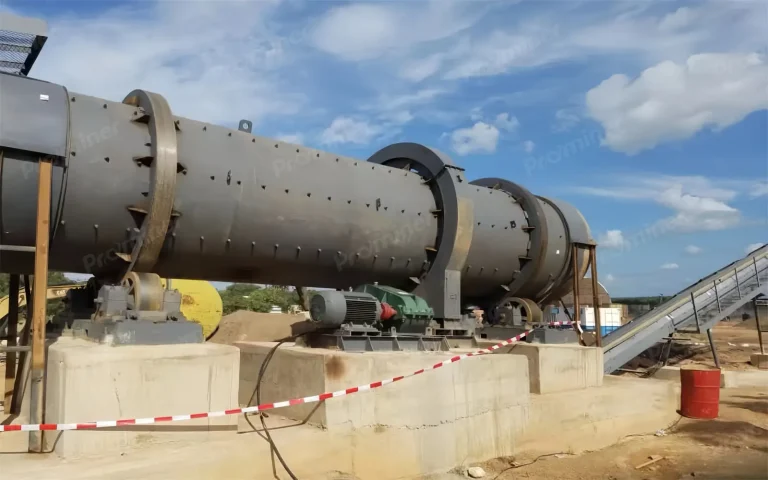
Heap leaching is a traditional cyanide leaching processing way which is flexible and economic to extract gold
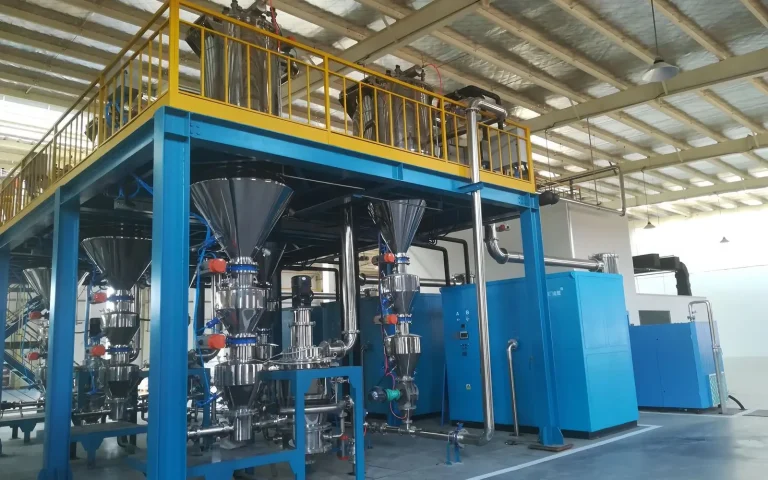
Silicon based anode is one kind of composite anode material by compounding silicon

Raw Ore: Alluvial/Sulfide Type Gold Ore (depending on specific deposit) Gold Grade: 3.5 g/t Gold Recovery Rate: 92%
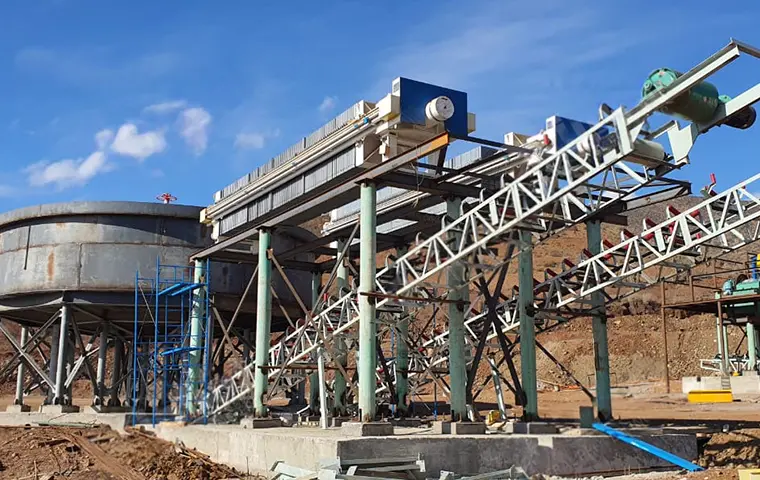
From laboratory testing to final commissioning, Prominer delivered a customized 20 TPH solution
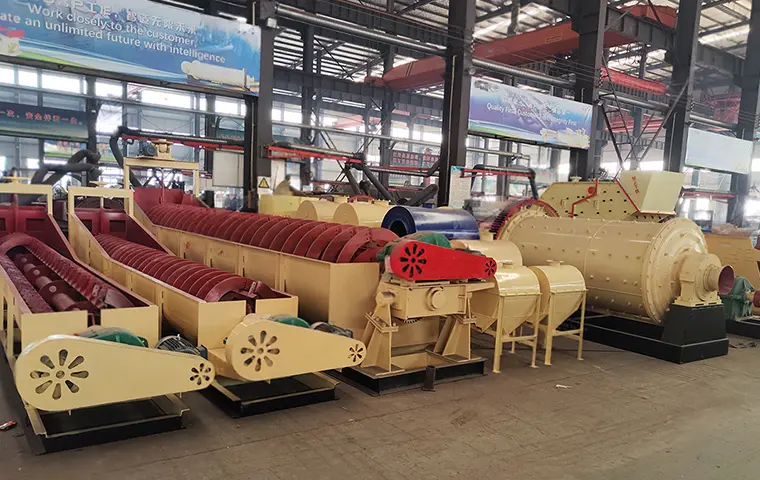
Raw Ore: Alluvial Gold Ore & Primary Hard Rock Gold Ore (Mixed Feed Capability) Feed Gold Grade: 1.2 – 3.5 g/t (variable)
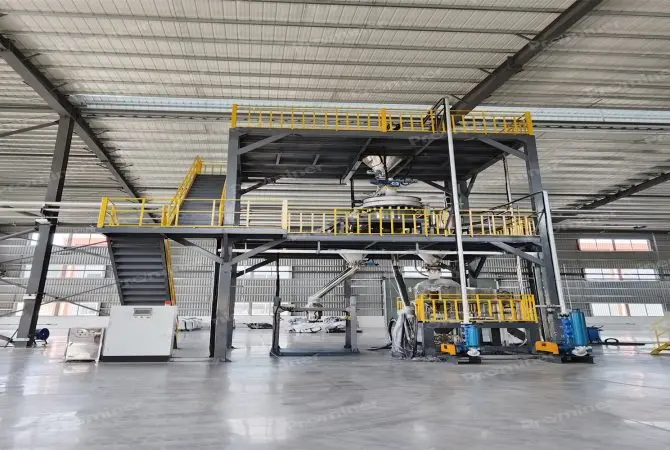
Raw Material: Artificial graphite anode, Natural graphite anode
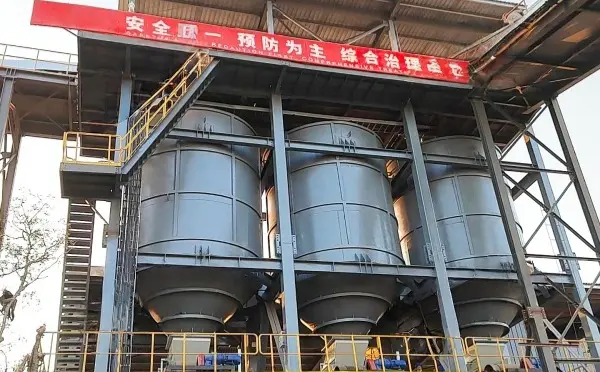
Raw Ore: Lepidolite, Spodumene, Gangue minerals: Quartz, Feldspar, Mica Li₂O Grade: 0.8%
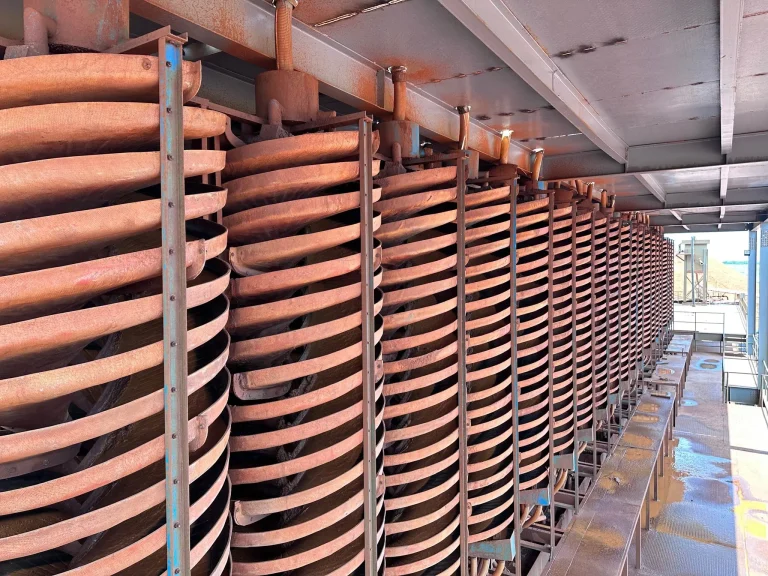
Raw Ore: Titanium Zirconium Beach Sand Ore TiO₂ Grade: 4.5% ZrO₂ Grade: 3.2%
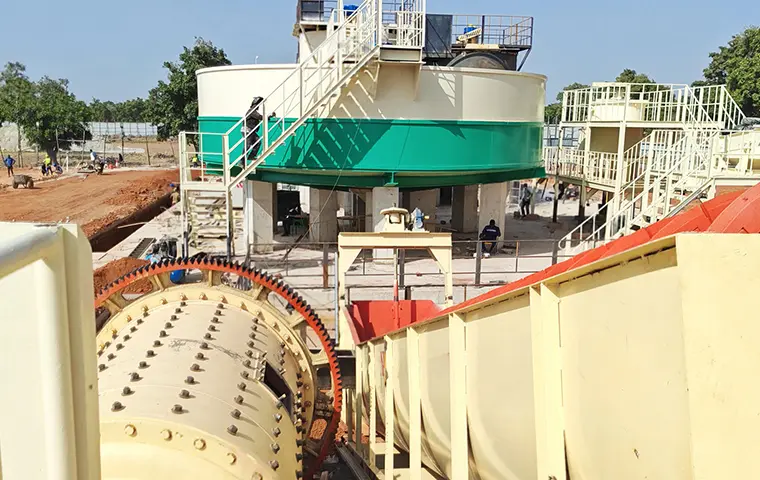
Raw Ore: Oxide and Sulfide Type Gold Ore Gold Grade: 2.5 g/t Final Product: Gold Bullion
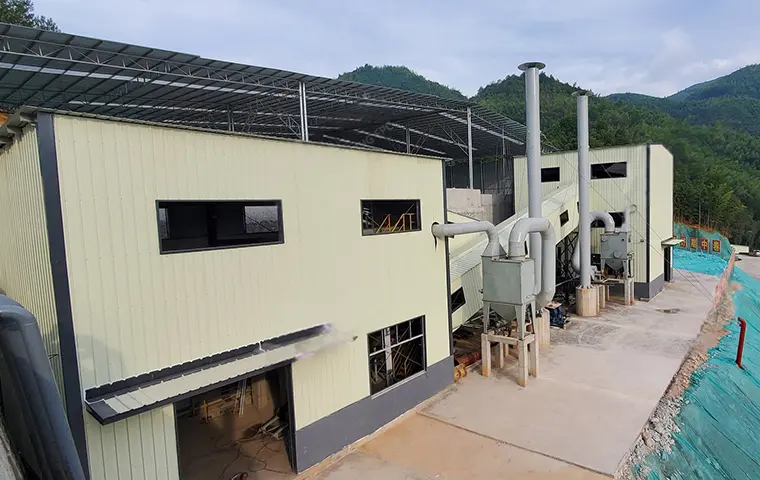
Raw Ore: High-Grade Fluorite Ore from Deep Veins Fluorspar Grade: 38% CaF₂ Concentrate Grade: 97.2% CaF₂
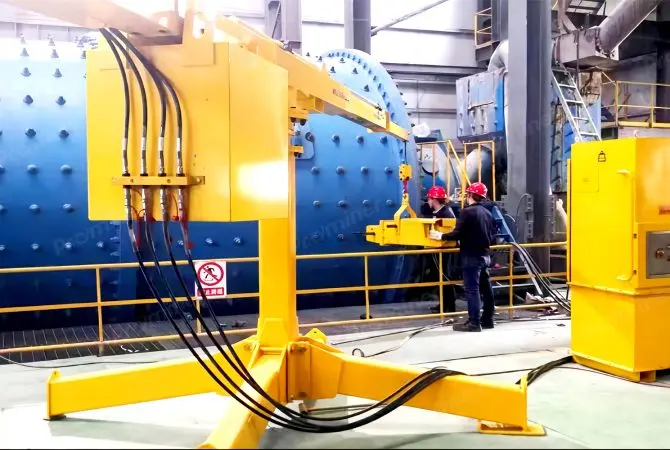
We can manufacture the highly automated and powerful recoilless Bolt Hammer to remove
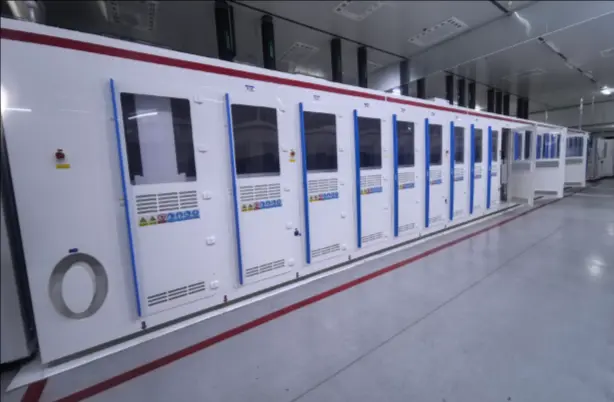
Include: Monocrystalline Batch Texturing Equipment, Batch Texturing Loader/Unloader, Low-Pressure…
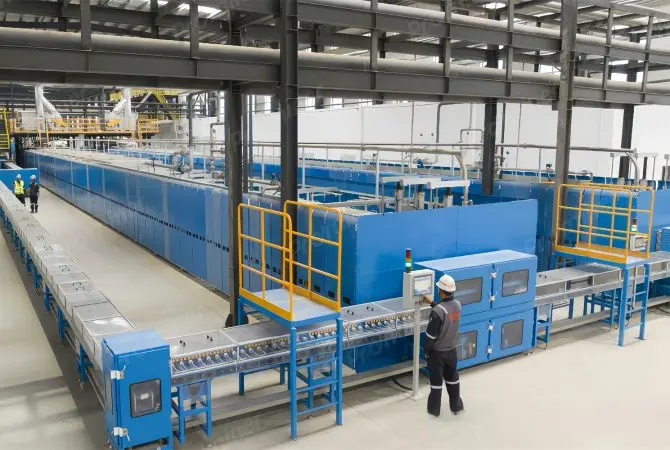
We can provide the complete solution for high temperature carbonization treatment system
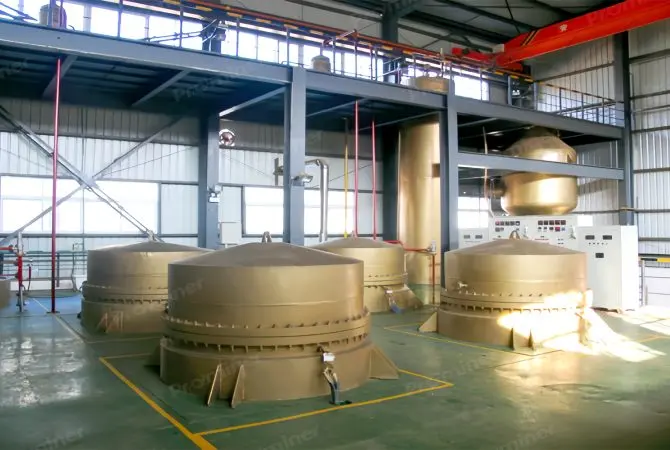
Prominer can design and provide the complete refinery and smelting system for gold CIL project
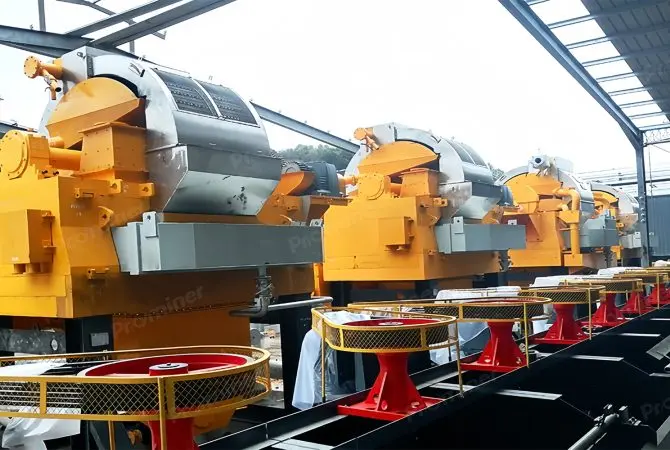
Prominer can provide different HIMS (High Intensity Magnetic separator) magnetic separators
To find out more about our products and solutions, please fll out the form below and one of our experts will get back to you shortly
3000 TPD Gold Flotation Project in Shandong Province
2500TPD Lithium Ore Flotation in Sichuan
Fax: (+86) 021-58779592
Address: Room 606, Building D3, Phase II, Chuansha Business Center, 777 Long, Miaochuan Road, Pudong New Area, Shanghai,China
Copyright © 2023. Prominer (Shanghai) Mining Technology Co.,Ltd.