UHP graphite electrode is mainly used for ultra high power electric arc furnaces in steel smelting industry

Iron ore processing aims to produce a higher-grade concentrate while minimizing energy use, water consumption, and waste. Two key methods that help achieve this are screening and flotation. Together, they improve plant efficiency by separating material more accurately and recovering valuable iron from lower-grade feed.
Screening is one of the first steps in iron ore processing. It separates ore by particle size, allowing oversized waste or fine material to be removed before further treatment.
This improves efficiency by:
By classifying ore early, screening helps plants focus processing capacity on material most likely to contain valuable iron.
Flotation is used to separate iron minerals from gangue based on differences in surface properties. It is especially useful for fine particles that are difficult to recover with gravity or magnetic separation alone.
In flotation:
This process boosts recovery from low-grade ores and tailings, increasing the overall iron yield from each ton of feed.
When screening and flotation are used together, they create a more efficient flowsheet. Screening removes coarse waste and controls feed size, while flotation recovers fine iron particles that would otherwise be lost.
The result is:
This combination helps operators maximize value from the ore body while lowering operating costs.
Flotation works best when the feed is properly prepared. Screening helps produce a more consistent particle size distribution, which improves reagent action and bubble-particle interaction in flotation cells.
A well-screened feed leads to:
In short, screening sets the stage for efficient flotation.
Flotation and screening improve iron ore processing efficiency by separating material more effectively at different stages of the plant. Screening reduces waste and prepares the feed, while flotation recovers fine iron particles that would otherwise be lost. Together, they help producers achieve higher recovery, lower costs, and better product quality.
A: The right process depends on your ore’s mineralogy, grade, particle size, and liberation characteristics — not on guesswork. The reliable way is to run laboratory and pilot tests first. These tests define whether flotation, gravity separation, magnetic separation, or leaching (or a combination) will deliver the best recovery and grade. We start every project with ore characterization and bench-scale tests, then scale up to pilot validation before committing to plant design — a testing-first approach that avoids costly process mistakes later.
A: Reagent selection depends on the mineral’s surface chemistry and the ore’s gangue composition. Collectors, frothers, depressants, and modifiers are chosen — and their dosages fine-tuned — through laboratory flotation tests on your actual ore sample, not from generic recipes. Over- or under-dosing both hurt recovery. Our metallurgical lab tests reagents on your ore to lock in the right combination and dosage before plant-scale operation, then re-optimizes during commissioning.
A: Heap leaching suits low-grade, high-tonnage ores — crushed ore is stacked and irrigated with a leaching solution, giving low capital and operating cost but slower, weather-dependent recovery. CIL (carbon-in-leach) and CIP (carbon-in-pulp) both use cyanide solution and activated carbon, but differ in where adsorption happens: CIL adds carbon during leaching, which suits clayey or high-fines ores; CIP adds carbon after leaching, which suits clean, free-filtering pulps. The choice comes down to ore type, grade, and throughput — we evaluate all three against your ore to recommend the most economical route.
A: Start by diagnosing where the loss occurs — usually in grinding, classification, or the separation stage itself. Common levers include: optimizing grind size for better liberation, upgrading to more efficient separation equipment (flotation cells, magnetic separators, spirals), automating control for steadier operation, and re-running metallurgical tests when the ore type changes. A structured audit plus targeted equipment or process upgrades typically recovers 2–5% more metal. We provide exactly this — process audits, equipment upgrades, and full EPC retrofits — to lift both recovery and grade.
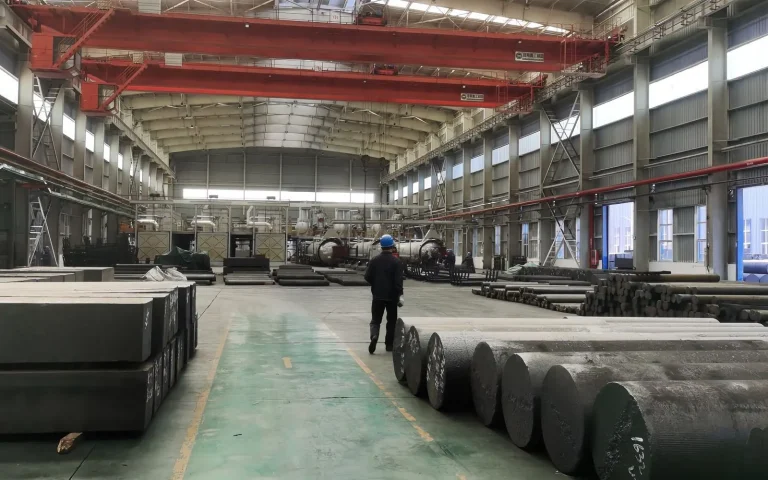
UHP graphite electrode is mainly used for ultra high power electric arc furnaces in steel smelting industry
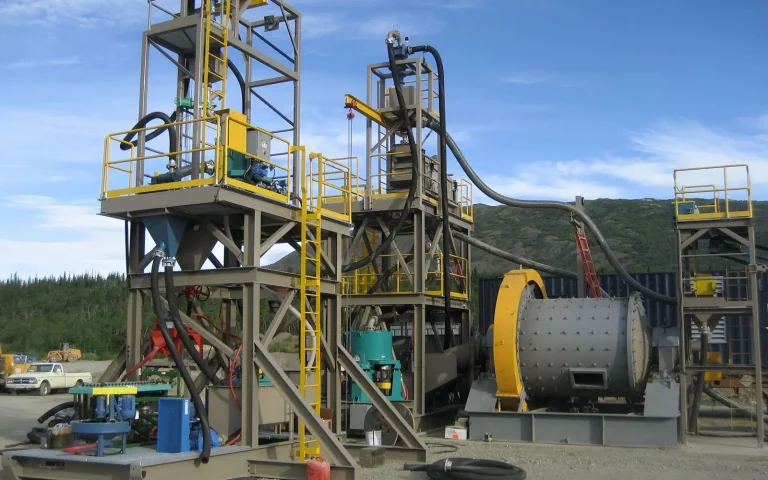
The best-known of the exogenetic ores is alluvial gold which also called placer gold. Alluvial gold refers
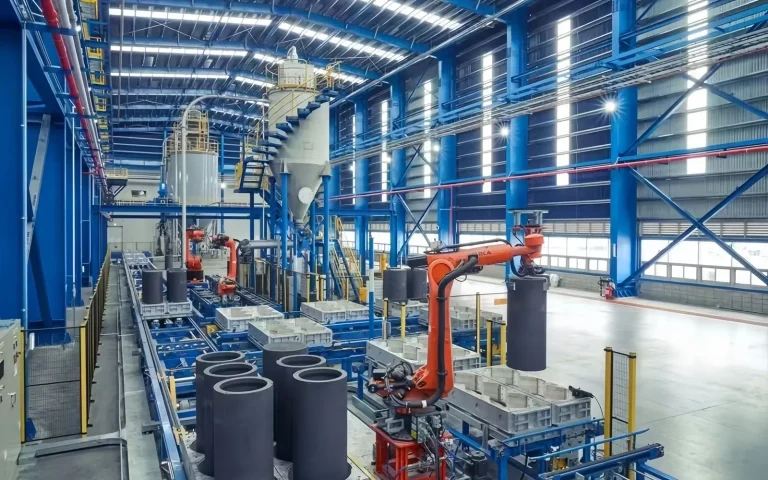
Prominer can provide the complete solution for making natrual graphite anode materials include grinding

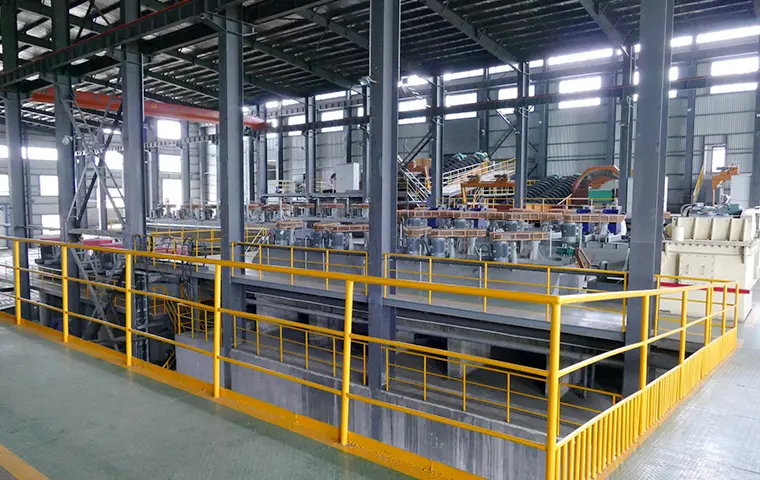
Raw Material: Spherical Graphite, Pitch Binder, Additives Project Capacity: 5,000 tons anode material; 20 tons graphene per annum
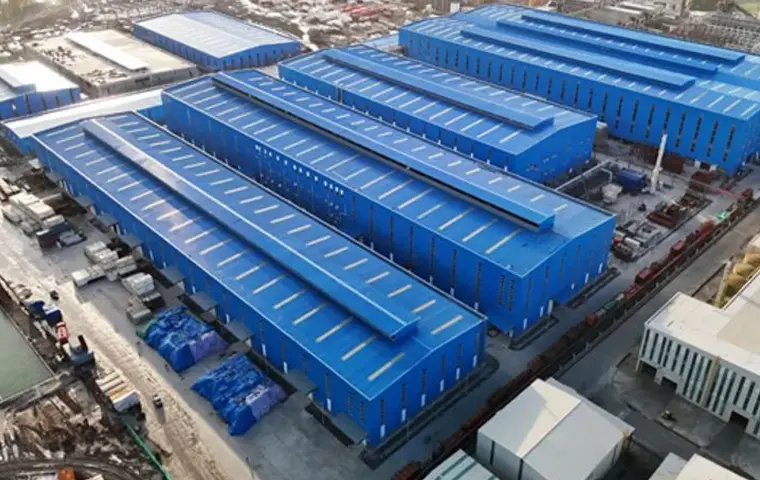
Raw Material: Petroleum Coke, Needle Coke, Pitch Binder Project Capacity: 50,000 Tons Per Annum
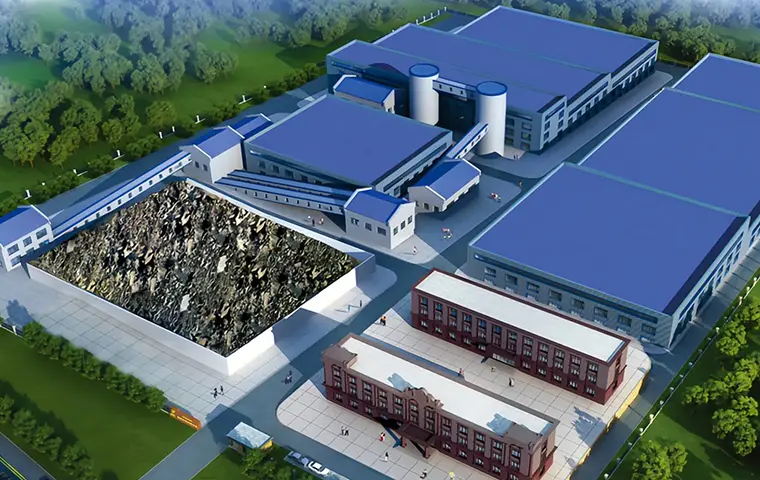
Raw Material: Natural Graphite Ore Concentrate Grade: 95% C TGC Final Product: Graphite Flotation Concentrate
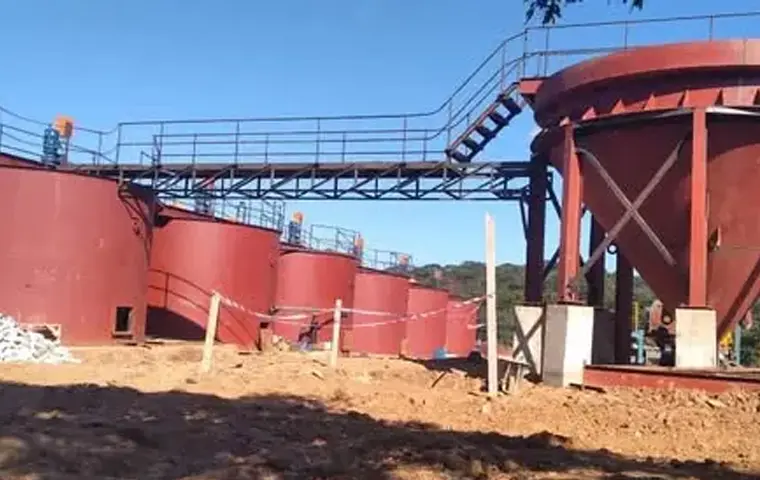
Raw Ore: Clay-rich oxidized gold ore (with minor sulfides) Gold Grade: 2.8 g/t Gold Ingot Purity: 89.5%
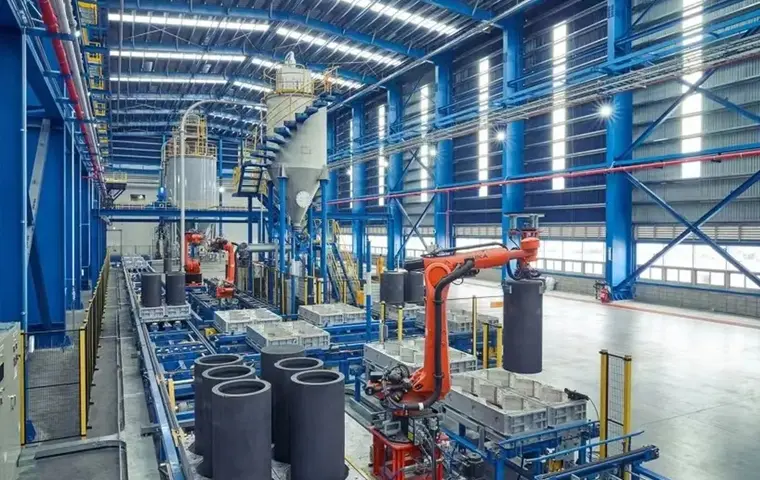
Raw Material: Green Petroleum Coke, Green Needle Coke and High soft point pitch
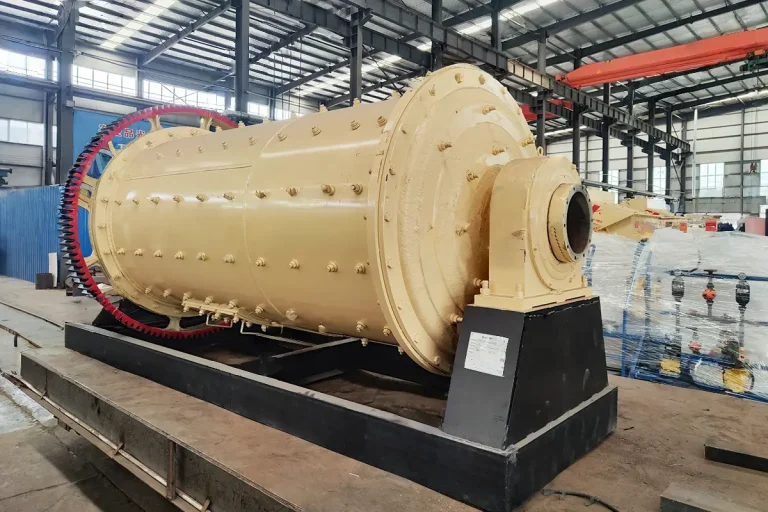
Raw Ore: Copper Ore (Chalcopyrite) Copper Grade: 0.85% Final Products: Grinded ore slurry for flotation
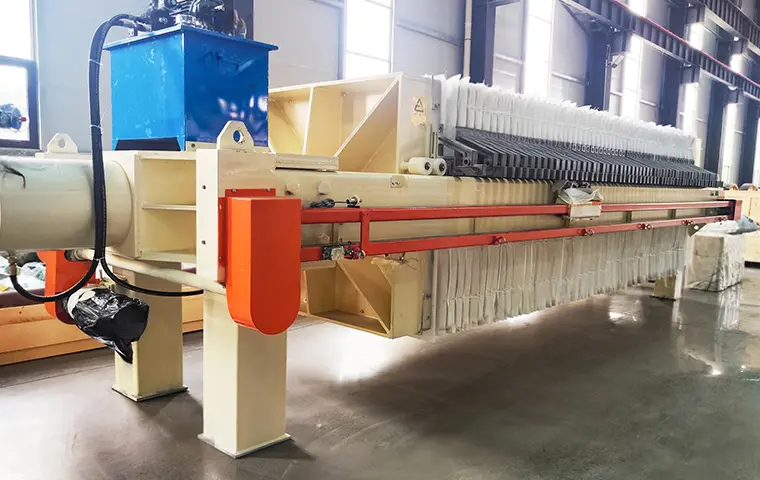
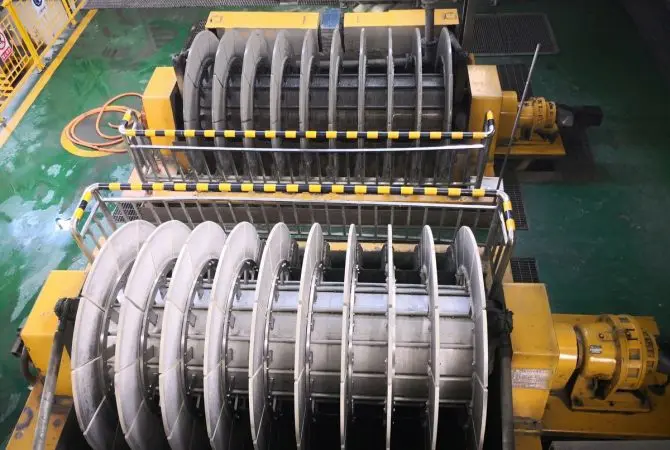
Project Background: Upgrade of dewatering circuit for flotation concentrate and plant tailings to reduce moisture content and enable dry stack disposal.
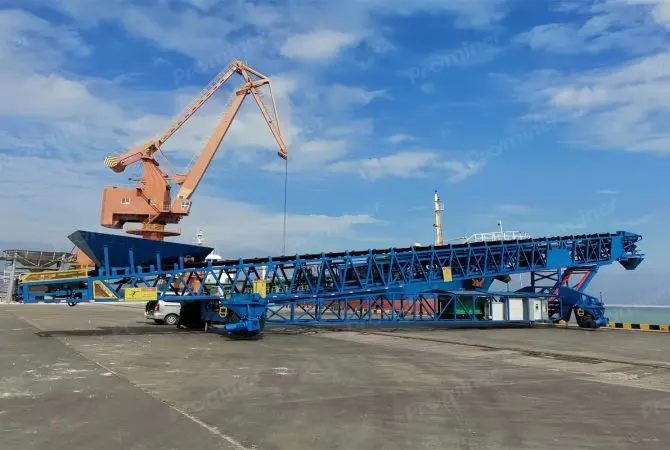
Our engineer team can design and manufacture the mobile type radial stacker, loader
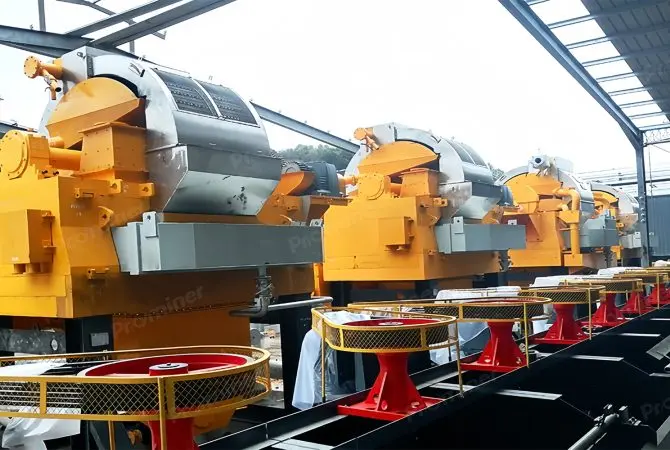
Prominer can provide different HIMS (High Intensity Magnetic separator) magnetic separators
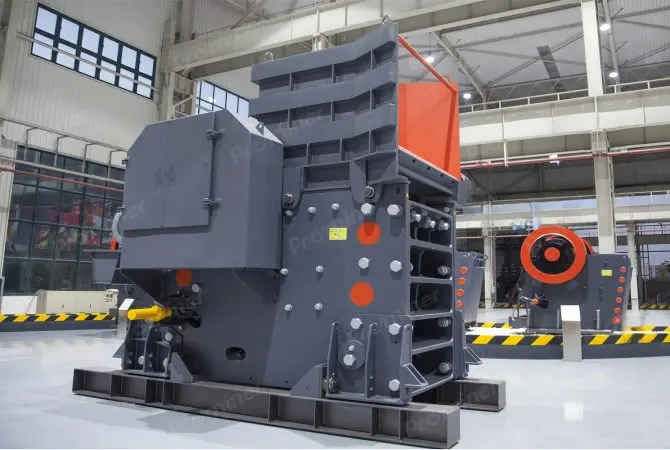
Jaw Crusher, its opening size determines its max feeding size. The crushing chamber of a jaw crusher
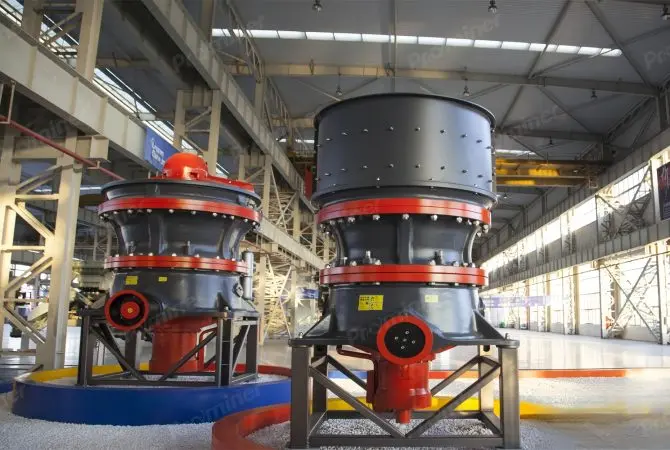
Single-cylinder hydraulic cone crusher have two series based on different cavity, S-cavity is designed
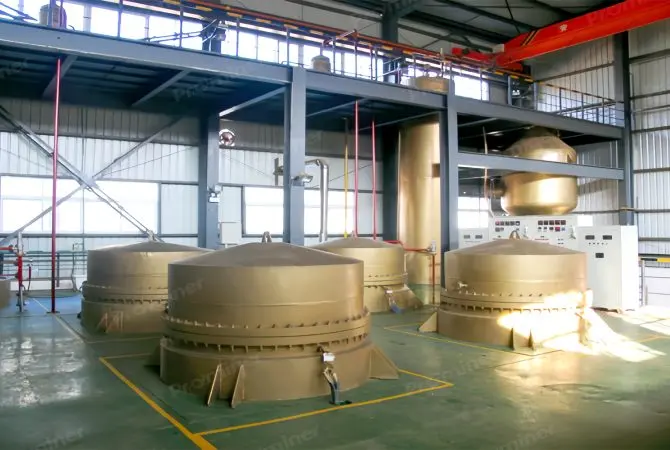
Prominer can design and provide the complete refinery and smelting system for gold CIL project
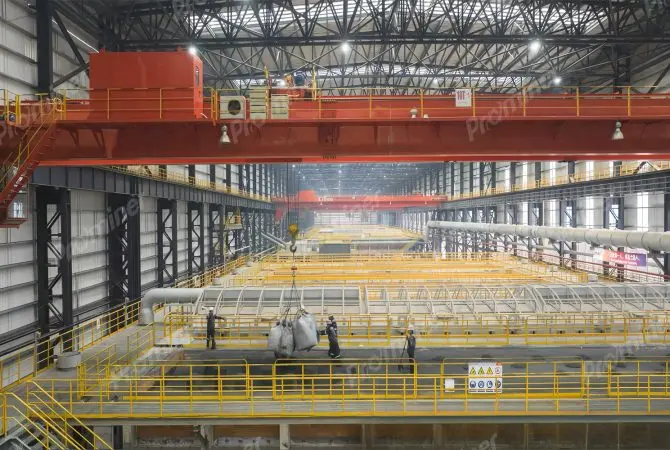
We can provide different type graphitization furnace for changing carbon material
To find out more about our products and solutions, please fll out the form below and one of our experts will get back to you shortly
3000 TPD Gold Flotation Project in Shandong Province
2500TPD Lithium Ore Flotation in Sichuan
Fax: (+86) 021-58779592
Address: Room 606, Building D3, Phase II, Chuansha Business Center, 777 Long, Miaochuan Road, Pudong New Area, Shanghai,China
Copyright © 2023. Prominer (Shanghai) Mining Technology Co.,Ltd.