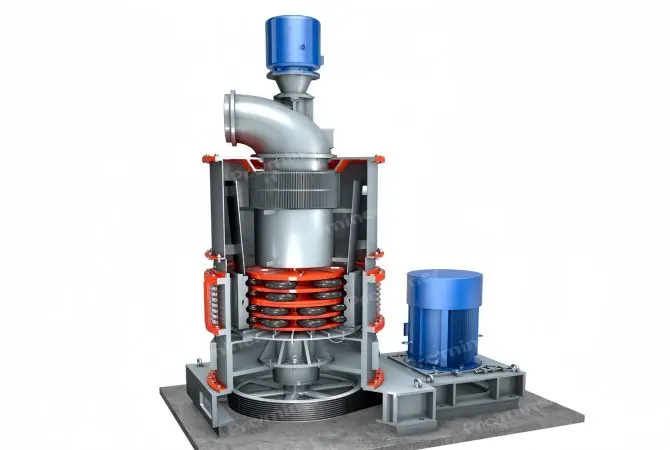

Provide the complete solution for making graphite anode materials include grinding, shaping, purification…
Gold heap leaching is highly sensitive to ore characteristics. Even when the process design is sound, ore properties can control solution flow, gold recovery, leach time, and reagent consumption.
Ore grade directly affects the economic performance of heap leaching. Higher gold content generally improves project returns, but the form of the gold matters just as much.
If gold is finely disseminated or locked in sulfides, cyanide may not access it easily. Free-milling gold usually leaches faster and more completely than refractory gold.
Particle size has a major influence on heap permeability and gold extraction.
A balance is needed: ore should be crushed enough to expose gold, but not so much that the heap becomes compacted.
Permeability determines how well leach solution moves through the heap. Poorly permeable ores create channeling, ponding, and uneven extraction.
Ores with high clay content, slimes, or weak rock structure often drain poorly. Good heap leaching ores maintain open pathways for irrigation and aeration.
Clay-rich ores can severely reduce heap performance.
Problems include:
These ores often require agglomeration or special stacking methods to maintain heap stability and solution flow.
Ore mineralogy affects both gold liberation and cyanide consumption.
Some minerals can consume cyanide or oxygen, lowering recovery efficiency. For example:
Understanding mineralogical composition is essential for predicting leach response.
Not all non-gold minerals are inert. Some gangue minerals react with leach reagents and increase operating costs.
Highly reactive ores may cause:
Testing ore reactivity helps estimate real leaching costs before heap construction.
Initial moisture and pore structure affect how solution distributes through the heap.
Well-porous ores allow better wetting and more uniform irrigation. Dense ores or ores with low internal porosity may resist solution penetration, causing incomplete gold recovery.
Ore deposits are rarely uniform. Changes in hardness, clay content, sulfide content, or grade can cause major fluctuations in heap performance.
Blending different ore types and consistent feed control can help stabilize leaching behavior and avoid recovery losses.
Ore properties strongly determine heap leaching success. Grade, mineralogy, particle size, permeability, and clay content all influence recovery, reagent use, and leach kinetics. Careful ore characterization and test work are essential for designing an efficient gold heap leach operation.
A: The right process depends on your ore’s mineralogy, grade, particle size, and liberation characteristics — not on guesswork. The reliable way is to run laboratory and pilot tests first. These tests define whether flotation, gravity separation, magnetic separation, or leaching (or a combination) will deliver the best recovery and grade. We start every project with ore characterization and bench-scale tests, then scale up to pilot validation before committing to plant design — a testing-first approach that avoids costly process mistakes later.
A: Reagent selection depends on the mineral’s surface chemistry and the ore’s gangue composition. Collectors, frothers, depressants, and modifiers are chosen — and their dosages fine-tuned — through laboratory flotation tests on your actual ore sample, not from generic recipes. Over- or under-dosing both hurt recovery. Our metallurgical lab tests reagents on your ore to lock in the right combination and dosage before plant-scale operation, then re-optimizes during commissioning.
A: Heap leaching suits low-grade, high-tonnage ores — crushed ore is stacked and irrigated with a leaching solution, giving low capital and operating cost but slower, weather-dependent recovery. CIL (carbon-in-leach) and CIP (carbon-in-pulp) both use cyanide solution and activated carbon, but differ in where adsorption happens: CIL adds carbon during leaching, which suits clayey or high-fines ores; CIP adds carbon after leaching, which suits clean, free-filtering pulps. The choice comes down to ore type, grade, and throughput — we evaluate all three against your ore to recommend the most economical route.
A: Start by diagnosing where the loss occurs — usually in grinding, classification, or the separation stage itself. Common levers include: optimizing grind size for better liberation, upgrading to more efficient separation equipment (flotation cells, magnetic separators, spirals), automating control for steadier operation, and re-running metallurgical tests when the ore type changes. A structured audit plus targeted equipment or process upgrades typically recovers 2–5% more metal. We provide exactly this — process audits, equipment upgrades, and full EPC retrofits — to lift both recovery and grade.
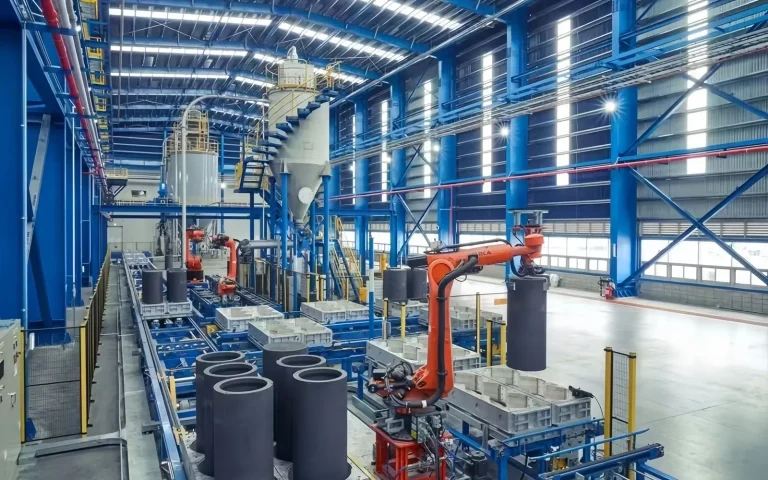
Provide the complete solution for making graphite anode materials include grinding, shaping, purification…
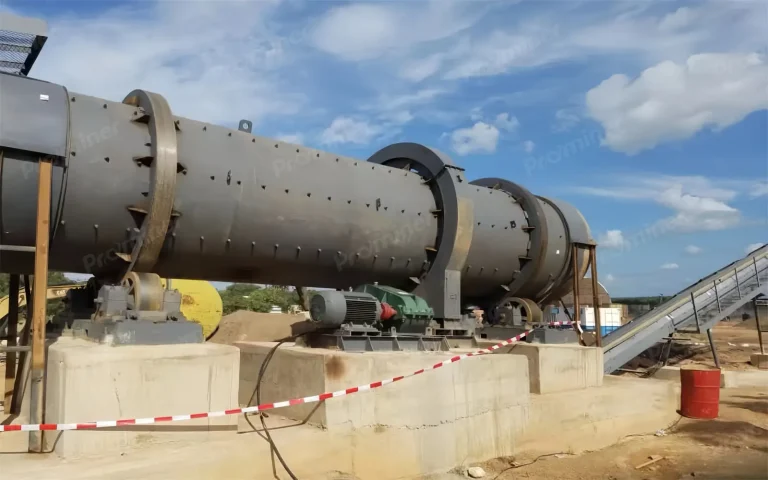
Heap leaching is a traditional cyanide leaching processing way which is flexible and economic to extract gold
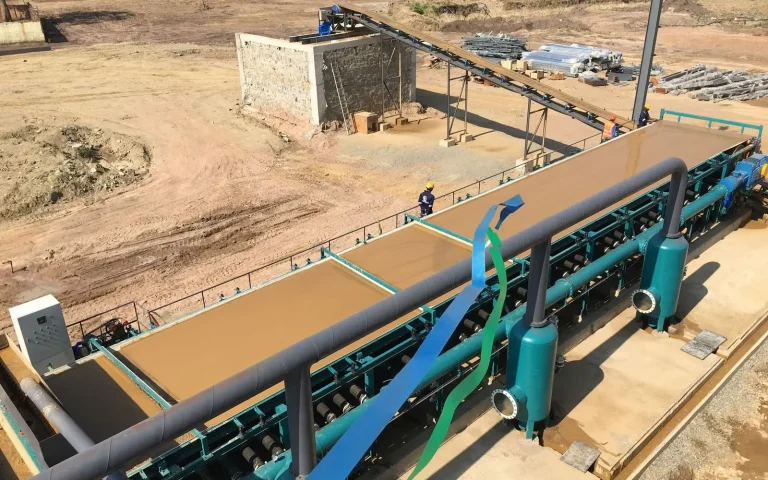
Gold CIL process (carbon in leaching) is very popular way to process the high grade oxide type gold ore

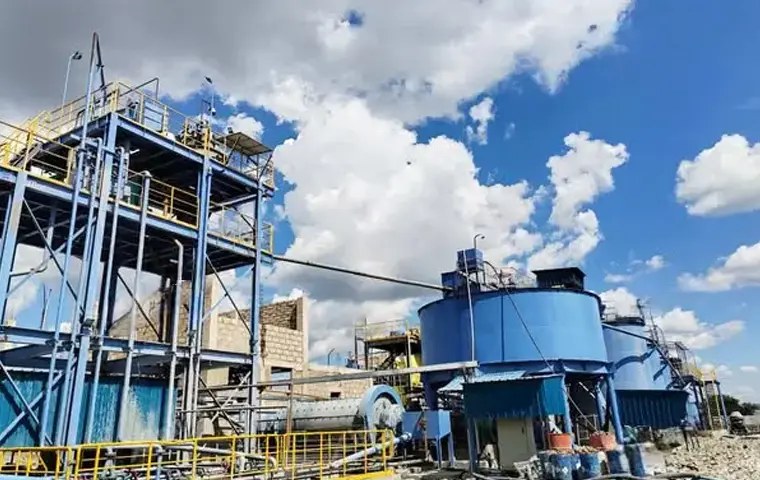
Raw Ore: Copper-Gold Ore Copper Grade: 1.2% Gold Grade: 1.5 g/t Recovery Rate: Copper 89%, Gold 88%
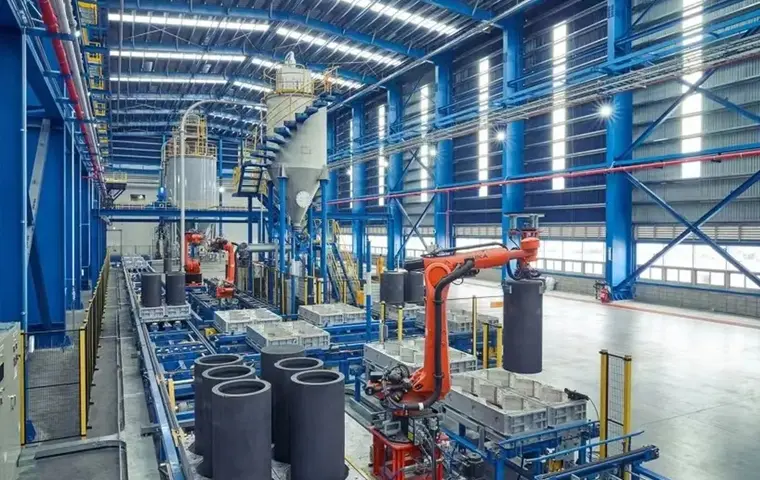
Raw Material: Green Petroleum Coke, Green Needle Coke and High soft point pitch
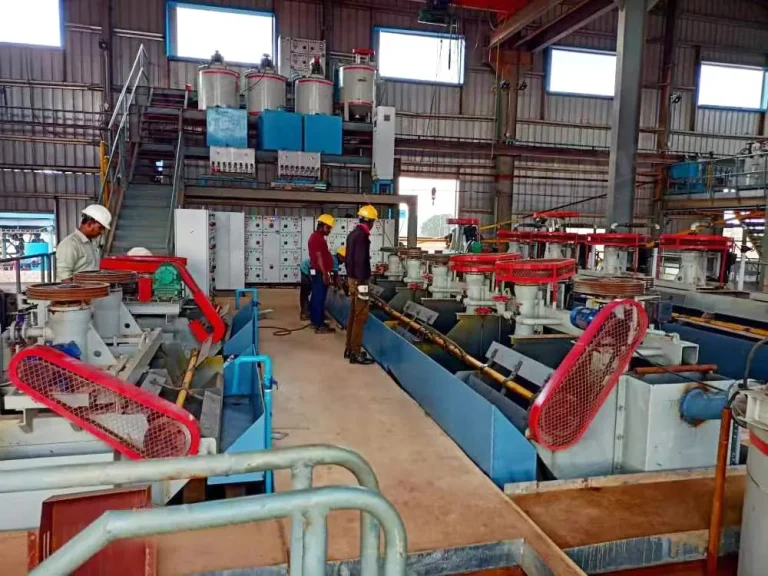
Raw Ore: Primary Sulfide Ore (Chalcopyrite-Bornite) Cu Grade: 0.72% Concentrate Grade: 28.3%
Capacity Target: Increase processing capacity from 500 TPD to 850 TPD in phases without halting production.
Raw Ore: Alluvial Gold with Magnetite & Hematite (Typical Sierra Madre Deposit)
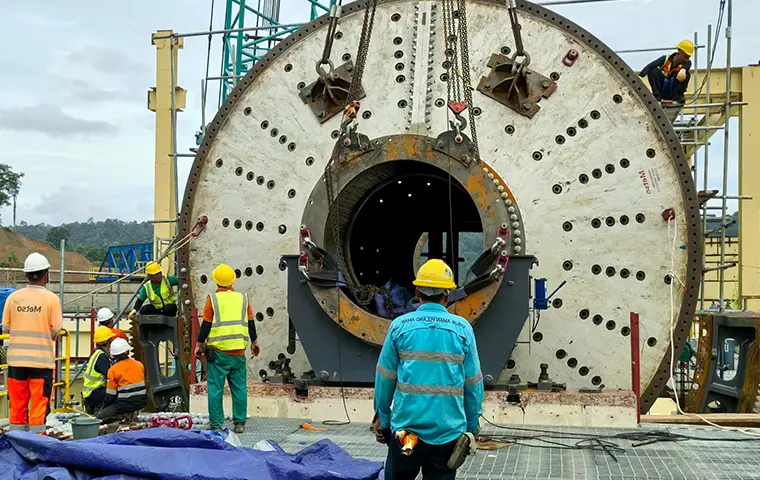
Raw Ore: Alluvial/Sulfide Type Gold Ore (depending on specific deposit) Gold Grade: 3.5 g/t Gold Recovery Rate: 92%
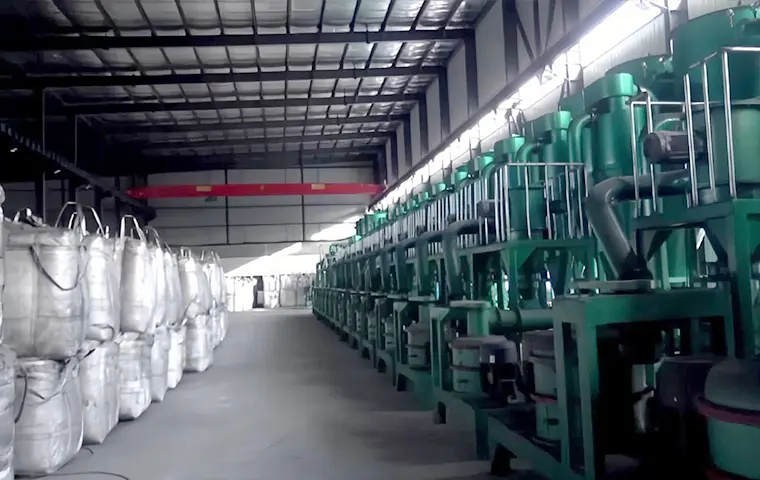
Raw Material: High-Purity Graphite (99.95% C) Project Capacity: 10,000 tons per annum
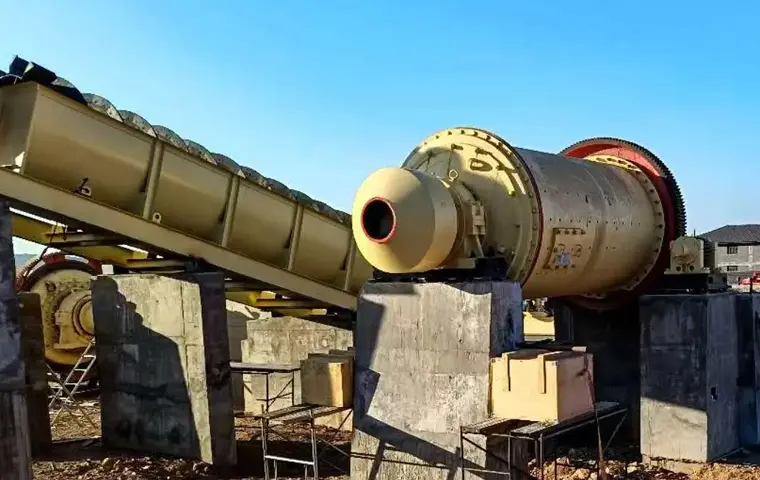
Raw Ore: Oxide Type Gold Ore Gold Grade: 2.5 g/t Gold Ingot Purity: 96%
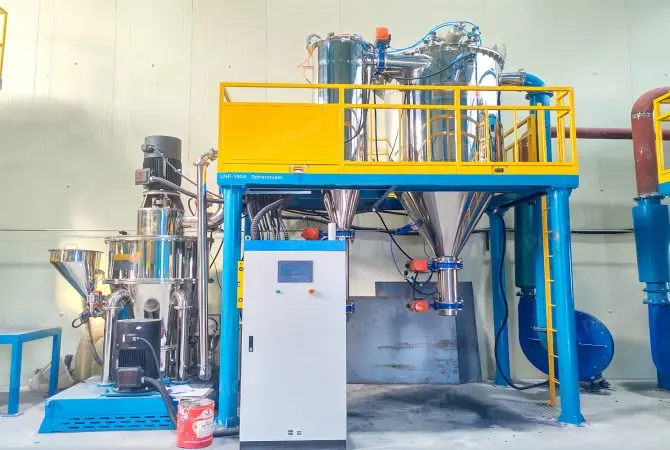
Besides strict PSD requirements, Anode Graphite also requires a spherical shape in order
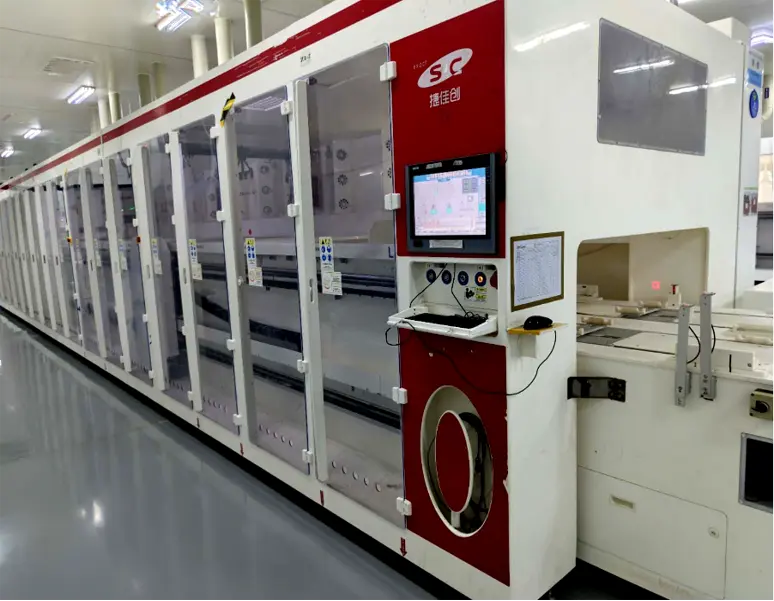
Such as: Boron diffusion furnace, BSG removal, Alkali polishing machine, PE-POLY…
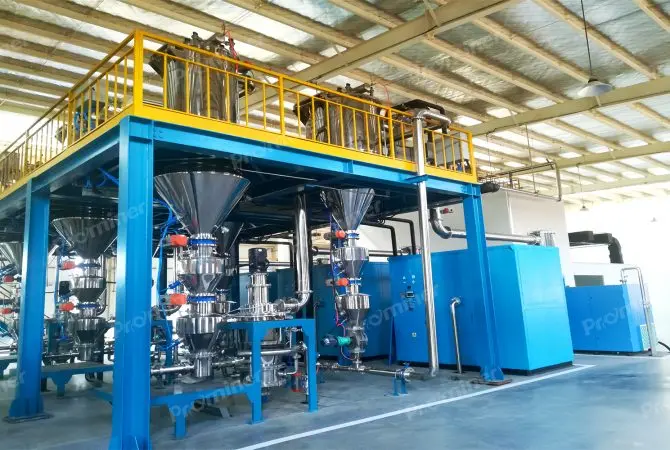
Jet mill is also called fluidized bed jet mill by using multiple nozzles to form sonic speed air flow
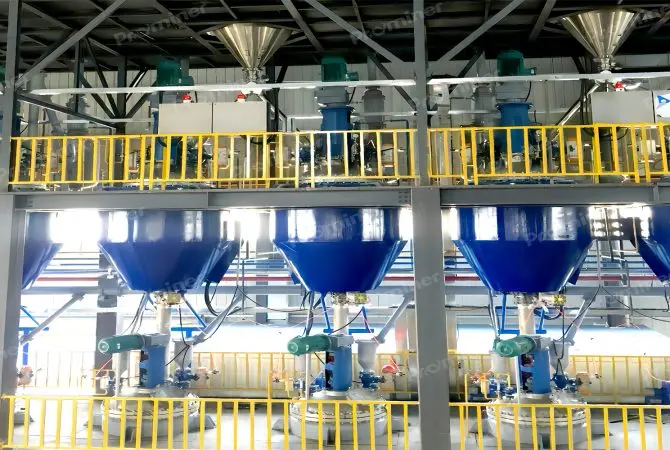
Our granulation reactor combines the coating and granulation processing functions together
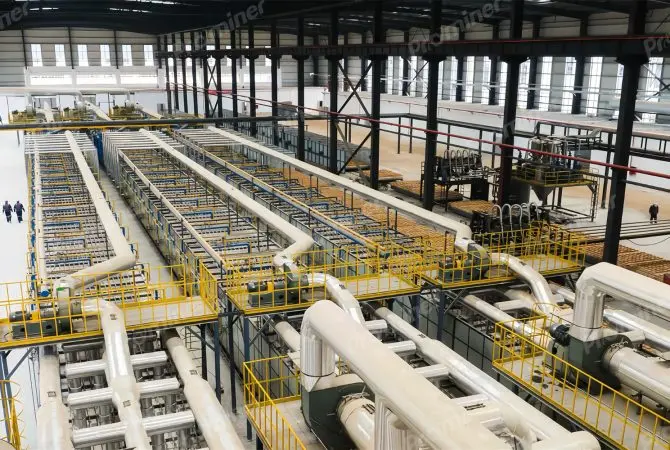
Prominer provides various types of furnaces for primary and secondary baking of carbon
To find out more about our products and solutions, please fll out the form below and one of our experts will get back to you shortly
3000 TPD Gold Flotation Project in Shandong Province
2500TPD Lithium Ore Flotation in Sichuan
Fax: (+86) 021-58779592
Address: Room 606, Building D3, Phase II, Chuansha Business Center, 777 Long, Miaochuan Road, Pudong New Area, Shanghai,China
Copyright © 2023. Prominer (Shanghai) Mining Technology Co.,Ltd.