Silicon based anode is one kind of composite anode material by compounding silicon

Designing a flowsheet for oxidized gold ore requires a careful understanding of the ore’s mineralogy, gold occurrence, gangue composition, and metallurgical behavior. Unlike refractory or sulfide-rich ores, oxidized gold ores are often more amenable to direct processing, but the best flowsheet still depends on ore variability, clay content, silver association, and the economics of recovery.
Below is a practical overview of how a flowsheet is typically developed for oxidized gold ore.
The starting point for any flowsheet design is a detailed characterization program. This includes:
Mineralogical analysis is essential because oxidized ores can host gold in several ways, including free-milling gold, gold associated with limonite or goethite, or fine gold trapped in residual quartz. These characteristics strongly influence the process route.
Once the ore is understood, the next step is deciding how gold will be recovered. For oxidized gold ore, the most common recovery options include:
The choice depends on ore grade, permeability, clay content, leach kinetics, and project scale. Low-grade, permeable ores often favor heap leaching, while higher-grade ores may justify crushing, grinding, and tank leaching.
A flowsheet must define how the ore is prepared for leaching or concentration. Oxidized gold ore is often softer than fresh sulfide ore, which can reduce grinding energy, but this is not always the case.
Typical comminution steps may include:
For heap leach operations, crushing may only be needed to achieve a suitable top size for permeability and gold exposure. For tank leaching, the ore may need grinding to a much finer size to maximize extraction.
If testwork shows a significant portion of the gold is coarse and liberated, gravity recovery can be added early in the flowsheet. This can improve overall recovery and reduce cyanide consumption by removing free gold before leaching.
Gravity recovery options may include:
A gravity circuit is especially useful when the ore contains visible gold or a recoverable coarse fraction.
Leaching is usually the core step in an oxidized gold ore flowsheet. The main methods are heap leaching and agitated leaching.
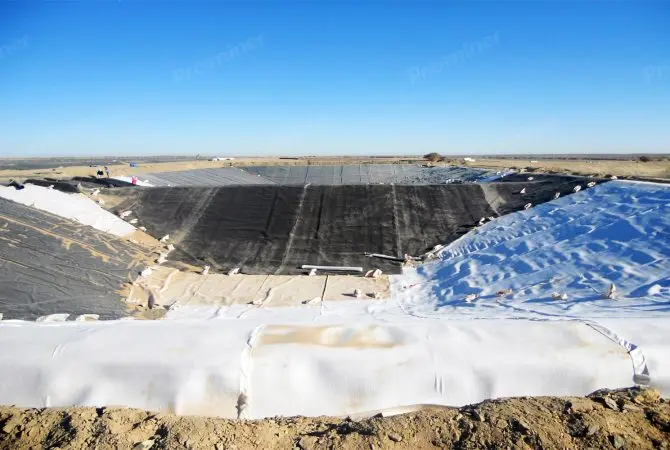
Heap leaching is commonly selected for low-grade oxidized ore because of its lower capital and operating cost. The flowsheet usually includes:
Heap leaching works best when the ore has good permeability and acceptable leach kinetics.
Agitated leaching is chosen when higher recoveries are needed or when the ore is not suitable for heaps. This route typically includes:
This approach usually gives faster leaching and potentially higher recovery, but with higher capital cost.
After leaching, dissolved gold must be recovered from solution or slurry. The three most common options are:
In CIP, leaching occurs first, followed by adsorption of dissolved gold onto activated carbon. This method is widely used when leach kinetics and adsorption conditions are favorable.
In CIL, leaching and carbon adsorption occur simultaneously in the same train of tanks. This can simplify the circuit and reduce losses due to preg-robbing in some cases, although preg-robbing is less common in truly oxidized ores.
Merrill-Crowe uses zinc precipitation after solution clarification and deaeration. It is often selected when the ore contains significant silver and the pregnant solution is relatively clear. In some oxidized gold-silver ores, this method can outperform carbon-based recovery.
Some oxidized ores contain substantial clay or fine material, which can create major operational problems. These include:
If these issues are identified, the flowsheet may need additional steps such as:
Ignoring clay behavior can lead to serious underperformance, especially in heap leach operations.
An effective flowsheet must also account for water balance and reagent consumption. For oxidized gold ore, important reagents often include:
Water quality can also affect leach performance. High dissolved salts, copper, or carbonate content may alter reagent consumption and recovery, so these factors should be considered in design.
The final stages of the flowsheet involve converting loaded carbon or precipitate into doré. Depending on the recovery route, this may include:
These downstream steps should be matched to the expected production rate, impurity levels, and refining requirements.
No oxidized gold ore flowsheet should be finalized without laboratory and pilot-scale testing. Typical testwork includes:
Testwork provides the recovery data, reagent requirements, and operating conditions needed to build a reliable process design. It also helps identify risks before capital is committed.
The highest metallurgical recovery does not always produce the best project outcome. A flowsheet should be selected based on the balance between:
For example, a heap leach circuit may recover less gold than a milling and CIL plant, but still produce a better economic return for a low-grade deposit.
Depending on ore type, a few common flowsheet configurations are often considered:
Suitable for:
Main steps:
Suitable for:
Main steps:
Suitable for:
Main steps:
Suitable for:
Main steps:
Designing a flowsheet for oxidized gold ore is a process of matching ore characteristics with the most appropriate and economic treatment route. While oxidized ores are often simpler to process than refractory ores, success still depends on good testwork, attention to ore variability, and thoughtful selection of crushing, leaching, and gold recovery methods.
The best flowsheet is not a standard template. It is a site-specific solution built around the ore, the recovery target, and the economics of the project.
A: A handful of variables drive most of the variation in recovery and grade: grind size (liberation), pulp density, reagent type and dosage, residence time, pH, and — for magnetic separation — field intensity and feed rate. Changing one without adjusting the others usually backfires. The practical way to find your optimum is a structured test program: vary one parameter at a time on your actual ore and measure recovery and grade at each point. We run this kind of parameter study during lab and pilot testing, then carry the settings into the plant design and re-tune them during commissioning.
A: Three properties matter most: whether the valuable mineral is sulfide or oxide, how coarsely or finely it is disseminated in the gangue, and what gangue minerals accompany it. Coarse, high-density minerals respond well to gravity separation; magnetic minerals to magnetic separation; fine sulfide minerals to flotation; oxide or low-grade ores often to leaching. Many ores need a staged combination. Because two deposits carrying the same metal can behave completely differently, the flowsheet has to be built from your ore’s own test data — not copied from a similar project.
A: A single method rarely hits both target recovery and target grade when the ore contains multiple valuable minerals, spans a wide particle size range, or carries problematic gangue. Then a combined flowsheet is justified — for example, gravity pre-concentration to reject coarse waste early, magnetic separation ahead of flotation to remove magnetic minerals, or staged grinding and classification to liberate progressively. The added circuit costs more, but it usually pays back through higher overall recovery and lower reagent and energy consumption per tonne.
A: Refractory ores resist standard processing — gold locked inside sulfide minerals, ores that consume excessive reagents, carbonaceous ores that re-adsorb dissolved gold, fine or clay-rich ores that slime badly, or oxide ores that float poorly. Treatment usually adds a step ahead of or instead of the conventional circuit: finer grinding, oxidation pre-treatment, roasting, or a switch from flotation to leaching. Identifying the specific cause through diagnostic testwork is essential, because each cause has a different fix and the wrong one wastes capital.
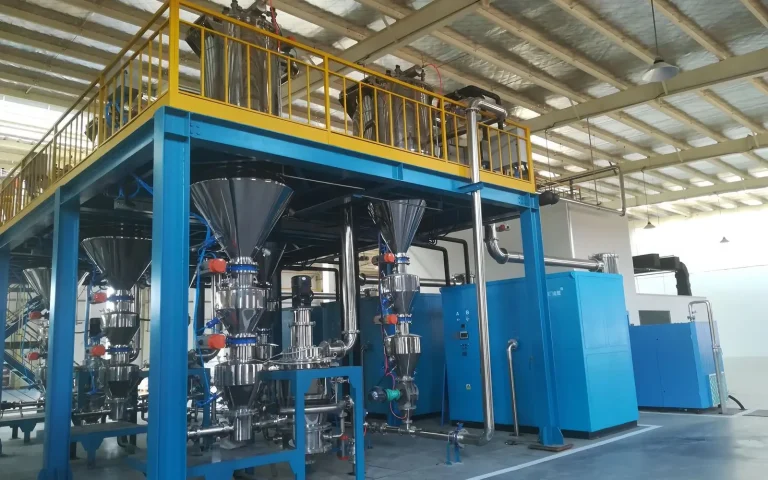
Silicon based anode is one kind of composite anode material by compounding silicon
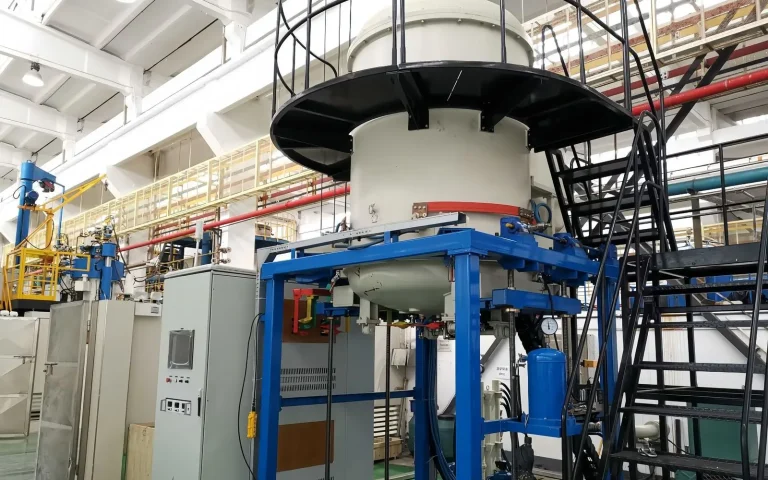
The demand from the industry over the years has been for special graphite and carbon with increasingly tighter
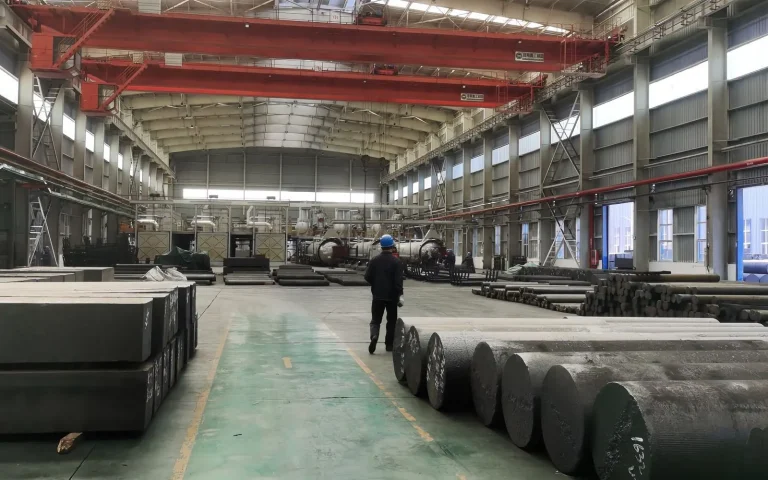
UHP graphite electrode is mainly used for ultra high power electric arc furnaces in steel smelting industry

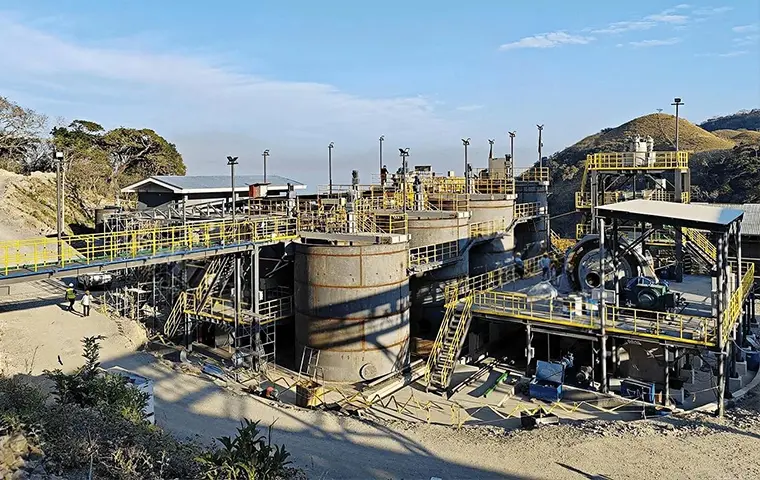
Raw Ore: Sulfide Type Copper Ore (Low-grade, heterogeneous) Feed Copper Grade: 0.45% Concentrate Copper Grade: 25%
Raw Ore: Complex phosphate ore with silica and carbonates P2O5 Grade: 18.5% Concentrate Grade: 32% P2O5
Raw Ore: High-Grade Crystalline Vein Graphite Ore Feed Grade: 18% C Concentrate Grade: 95% C (TGC)
Raw Ore: Sulfide-Bearing Gold Ore (30% Sulfide) Gold Grade: 3.2 g/t Final Product: 98.99% Gold Ingot

Raw Ore: Sulfide Type Copper Ore (with associated gold) Gold Grade: 0.6 g/t Copper Grade: 1.2%
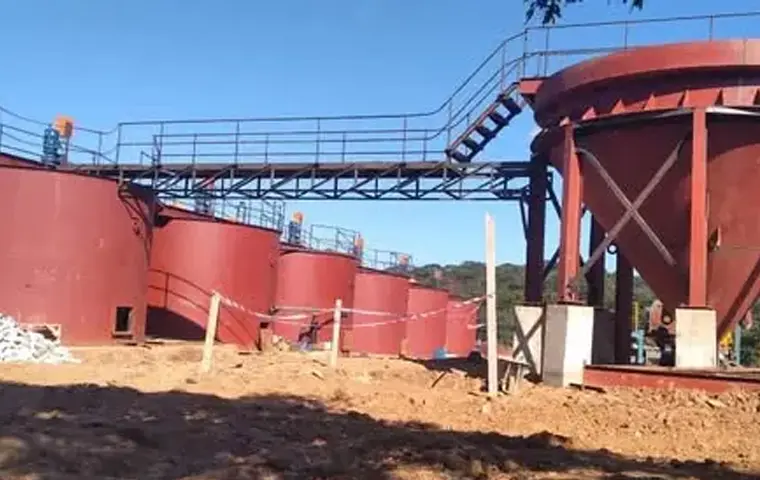
Raw Ore: Clay-rich oxidized gold ore (with minor sulfides) Gold Grade: 2.8 g/t Gold Ingot Purity: 89.5%
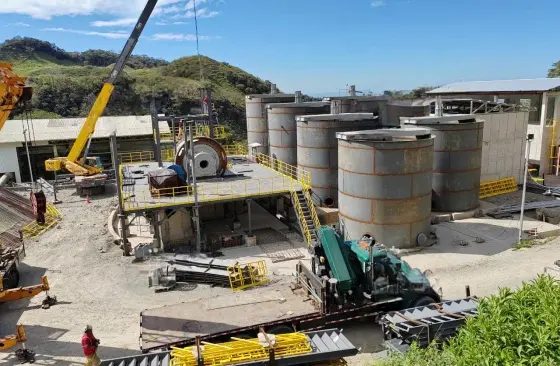
Raw Ore: Free-Milling Oxide Gold Ore Gold Grade: 1.5-3.5 g/t Final Product: Dore Gold Bar (Au+Ag≥90%)
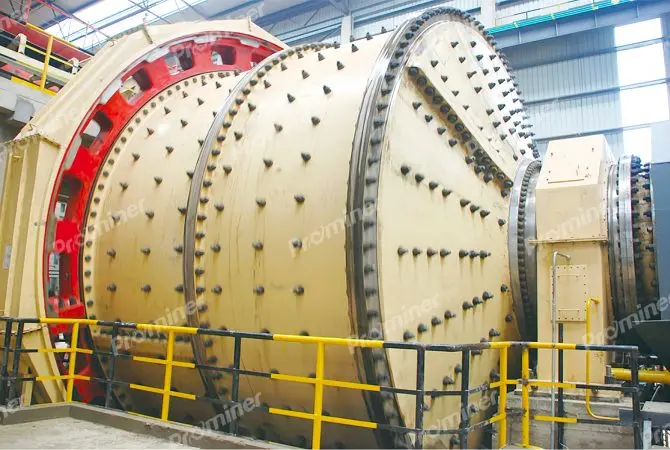
AG/SAG is short for autogenous mill and semi-autogenous mill, it combines with two functions of crushing
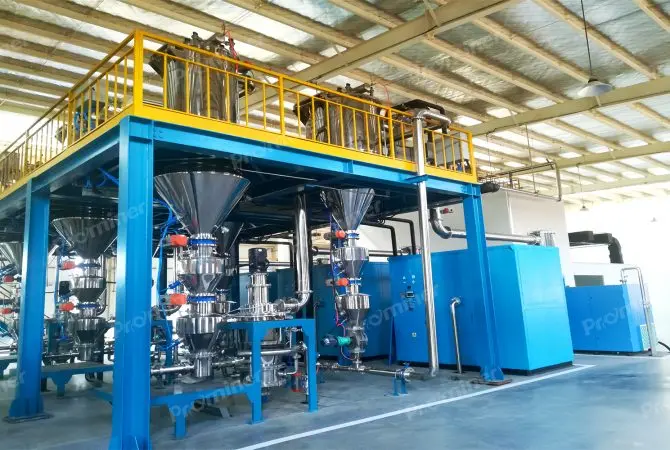
Jet mill is also called fluidized bed jet mill by using multiple nozzles to form sonic speed air flow
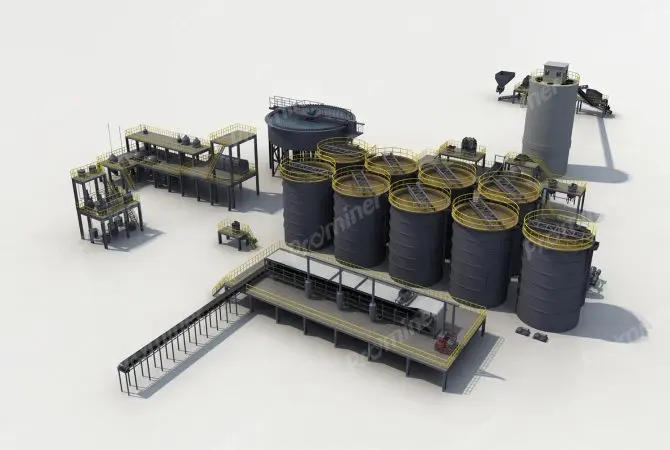
Prominer can provide the complete solution for CIL (carbon in leaching) system
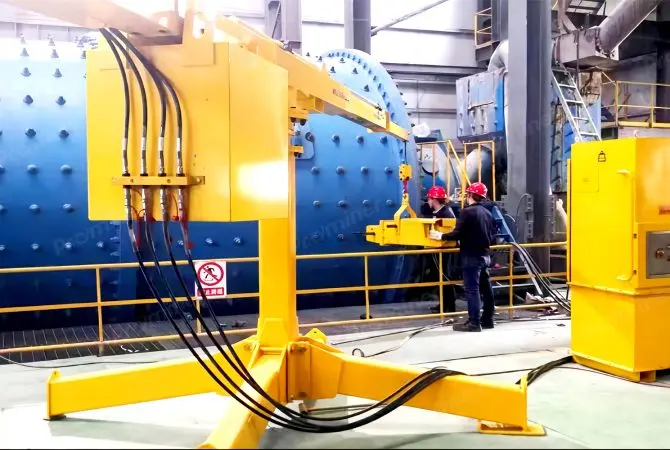
We can manufacture the highly automated and powerful recoilless Bolt Hammer to remove
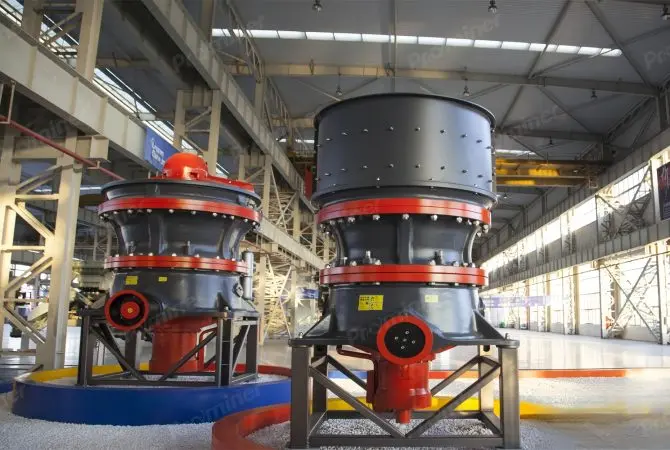
Single-cylinder hydraulic cone crusher have two series based on different cavity, S-cavity is designed
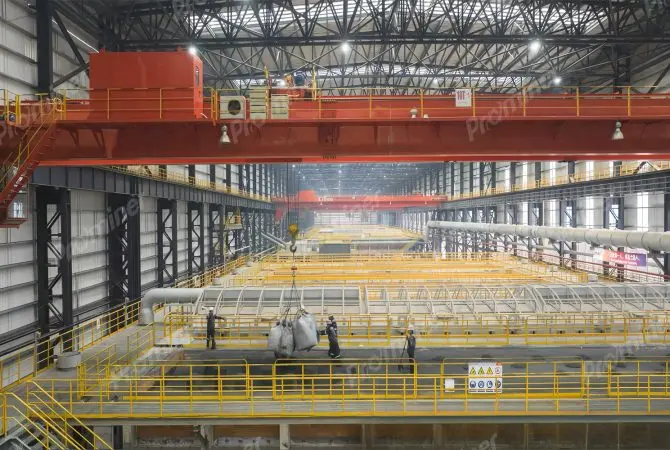
We can provide different type graphitization furnace for changing carbon material
To find out more about our products and solutions, please fll out the form below and one of our experts will get back to you shortly
3000 TPD Gold Flotation Project in Shandong Province
2500TPD Lithium Ore Flotation in Sichuan
Fax: (+86) 021-58779592
Address: Room 606, Building D3, Phase II, Chuansha Business Center, 777 Long, Miaochuan Road, Pudong New Area, Shanghai,China
Copyright © 2023. Prominer (Shanghai) Mining Technology Co.,Ltd.