There are two types natural graphite ore include crystalline graphite and amorphous graphite

Quartz-feldspar separation depends on the exact mineral mix, grain size, and degree of liberation. Before choosing reagents, identify:
A good reagent scheme starts with knowing what needs to be floated and what needs to be depressed.
Quartz and feldspar respond differently to collectors because their surface charges and active sites vary with pH. In acidic to neutral conditions, feldspar can often be floated while quartz is depressed, or vice versa depending on the circuit design.
Key factors include:
Collectors are the main reagents that make the target mineral hydrophobic. For quartz-feldspar separation, common collector choices include:
Selection should depend on which mineral you want to float, the water chemistry, and how clean the separation must be.
Depressants prevent unwanted minerals from floating. In quartz-feldspar circuits, they are often used to suppress quartz, feldspar, or gangue minerals.
Common depressant options:
The best depressant is one that improves selectivity without causing excessive recovery loss.
pH is one of the most important variables in flotation reagent performance. Even the best reagent can fail if the pulp chemistry is wrong.
Consider:
Always test reagents in the same water source used in the plant.
Bench-scale and pilot testing are essential before full-scale selection. Reagent performance can change sharply with ore variability.
Testing should measure:
Use staged testing to compare collectors, depressants, and pH conditions systematically.
The best flotation reagent is not always the one that gives the highest recovery. In quartz-feldspar separation, the goal is usually high-purity concentrate with acceptable yield.
A strong reagent scheme should:
Typical mistakes include:
Careful reagent optimization usually saves more cost than chasing a single “universal” reagent.
Choosing the right flotation reagents for quartz-feldspar separation requires understanding the ore, controlling pulp chemistry, and testing multiple reagent combinations. The best solution is usually site-specific, based on mineralogy, pH, water quality, and target product specifications. A systematic approach leads to better recovery, cleaner concentrate, and lower operating costs.
A: The right process depends on your ore’s mineralogy, grade, particle size, and liberation characteristics — not on guesswork. The reliable way is to run laboratory and pilot tests first. These tests define whether flotation, gravity separation, magnetic separation, or leaching (or a combination) will deliver the best recovery and grade. We start every project with ore characterization and bench-scale tests, then scale up to pilot validation before committing to plant design — a testing-first approach that avoids costly process mistakes later.
A: Reagent selection depends on the mineral’s surface chemistry and the ore’s gangue composition. Collectors, frothers, depressants, and modifiers are chosen — and their dosages fine-tuned — through laboratory flotation tests on your actual ore sample, not from generic recipes. Over- or under-dosing both hurt recovery. Our metallurgical lab tests reagents on your ore to lock in the right combination and dosage before plant-scale operation, then re-optimizes during commissioning.
A: Heap leaching suits low-grade, high-tonnage ores — crushed ore is stacked and irrigated with a leaching solution, giving low capital and operating cost but slower, weather-dependent recovery. CIL (carbon-in-leach) and CIP (carbon-in-pulp) both use cyanide solution and activated carbon, but differ in where adsorption happens: CIL adds carbon during leaching, which suits clayey or high-fines ores; CIP adds carbon after leaching, which suits clean, free-filtering pulps. The choice comes down to ore type, grade, and throughput — we evaluate all three against your ore to recommend the most economical route.
A: Start by diagnosing where the loss occurs — usually in grinding, classification, or the separation stage itself. Common levers include: optimizing grind size for better liberation, upgrading to more efficient separation equipment (flotation cells, magnetic separators, spirals), automating control for steadier operation, and re-running metallurgical tests when the ore type changes. A structured audit plus targeted equipment or process upgrades typically recovers 2–5% more metal. We provide exactly this — process audits, equipment upgrades, and full EPC retrofits — to lift both recovery and grade.
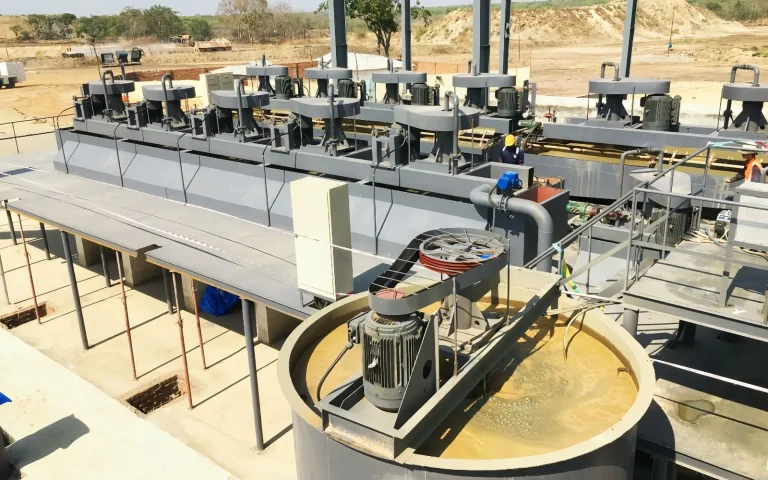
There are two types natural graphite ore include crystalline graphite and amorphous graphite
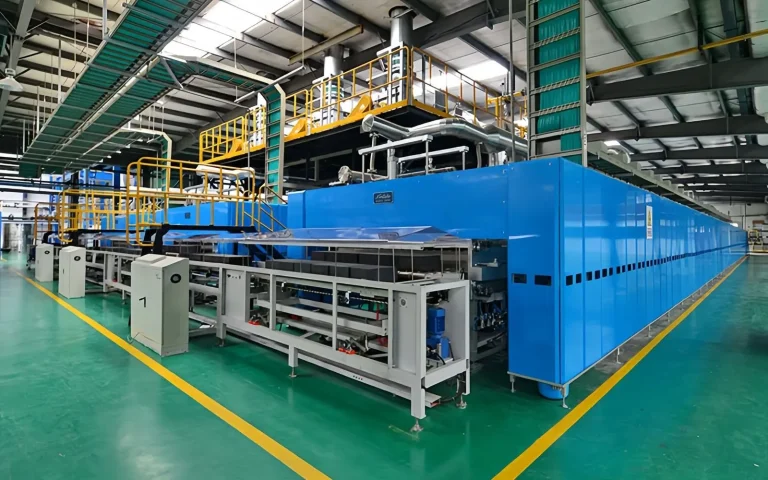
Artificial graphite anode material are mainly made from high quality low sulphur content petroleum coke
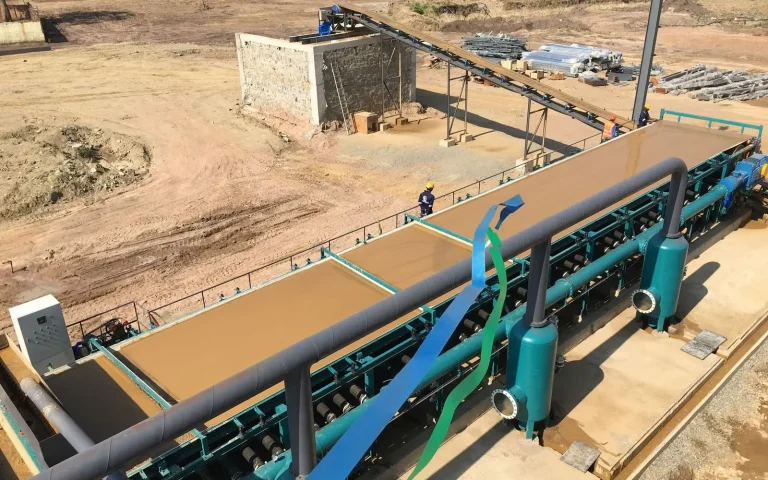
Gold CIL process (carbon in leaching) is very popular way to process the high grade oxide type gold ore

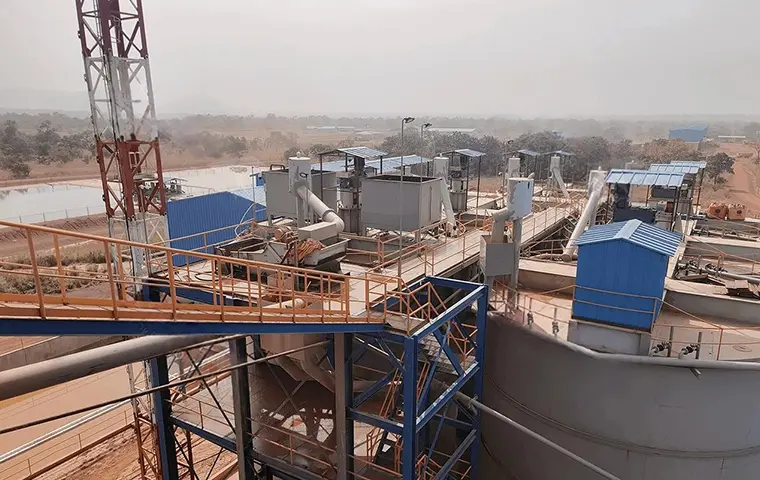
Raw Ore: Sulfide Copper Ore (with minor pyrite content) Copper Grade: 1.2% Concentrate Grade 25% Cu
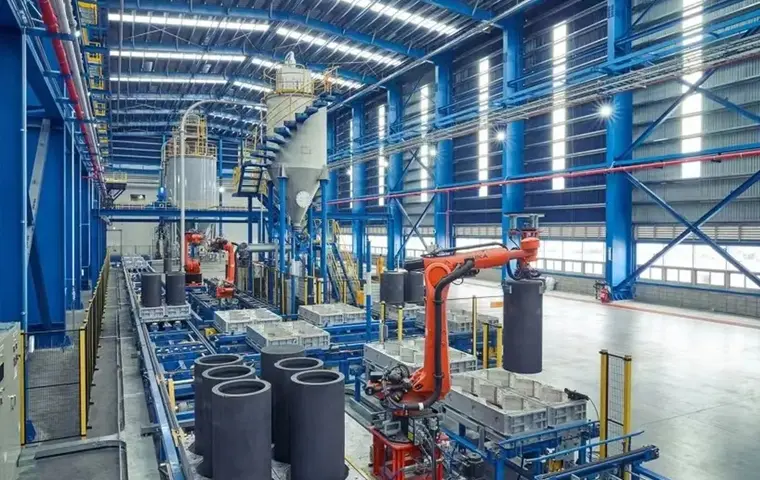
Raw Material: Green Petroleum Coke, Green Needle Coke and High soft point pitch
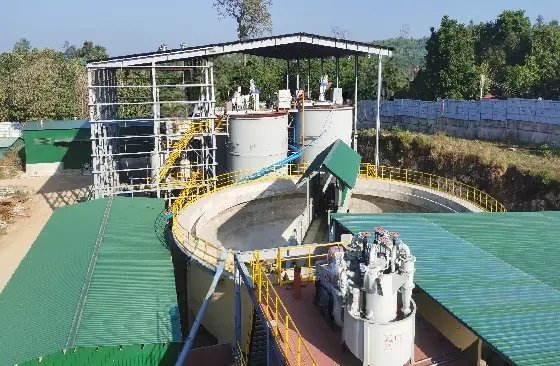
Location: Tanzania, Africa & Central Kalimantan, Indonesia Ore Type: Low-Grade Sulfide Ore (1.2–1.8 g/t Au)
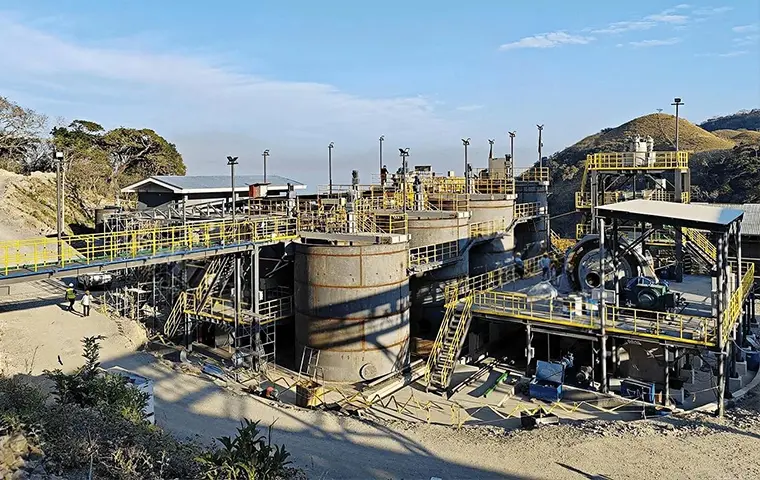
Raw Ore: Sulfide Type Copper Ore (Low-grade, heterogeneous) Feed Copper Grade: 0.45% Concentrate Copper Grade: 25%
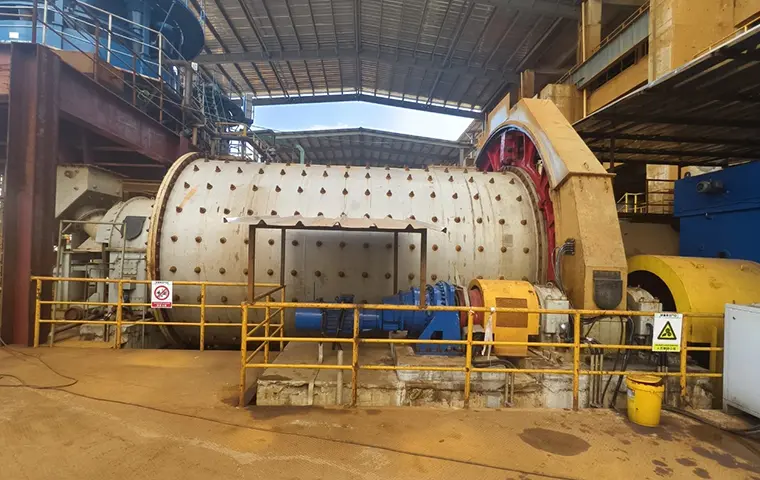
Located in Indonesia, this project focuses on the efficient regrinding of nickel ore to enhance mineral upgrading and deep processing. Prominer (Shanghai) Mining Technology Co., Ltd.
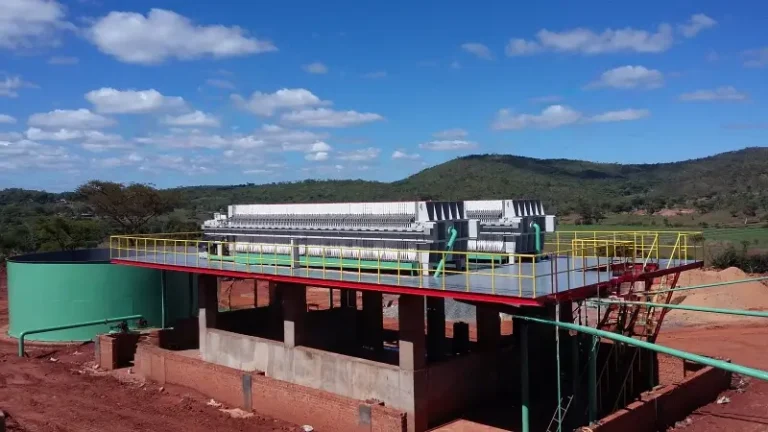
Raw Ore: Sulfide-Bearing Gold Ore (30% Sulfide) Gold Grade: 3.2 g/t Final Product: 98.99% Gold Ingot
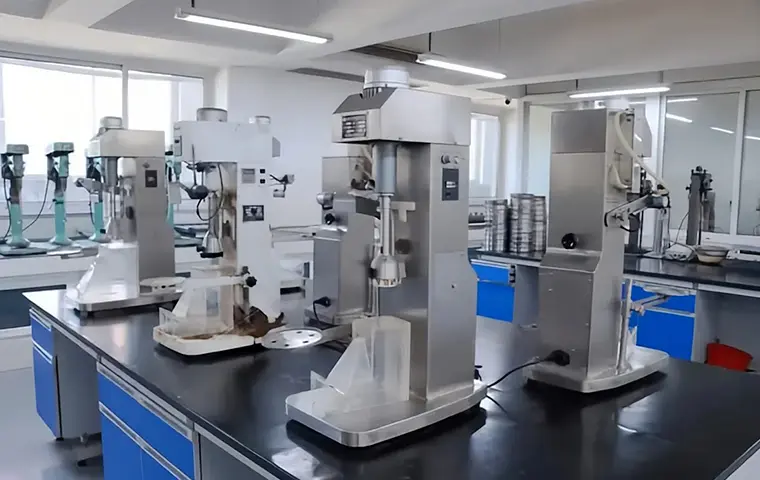
Raw Material: Various types of ore samples (gold, lithium, graphite, etc.) Lab Capacity: 50–100 samples per day
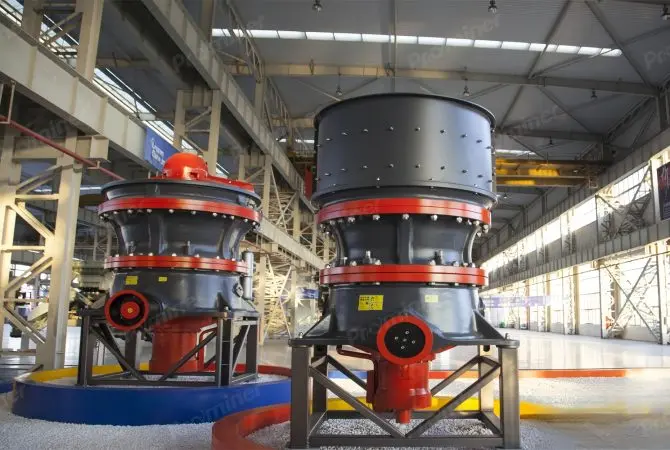
Single-cylinder hydraulic cone crusher have two series based on different cavity, S-cavity is designed
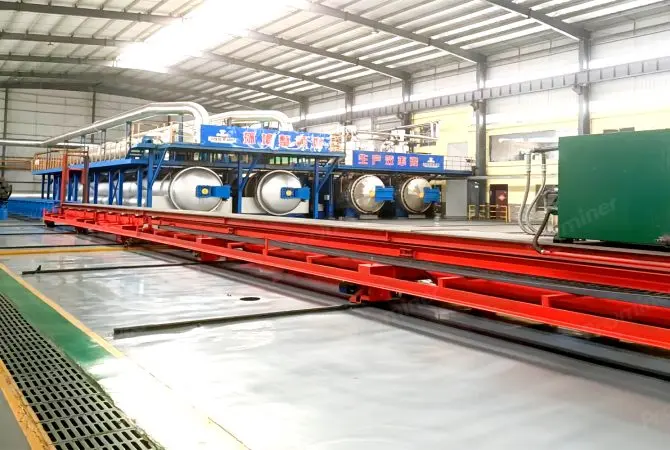
We can provide hot-in and cold-out type high-pressure impregnation of once-baked graphite
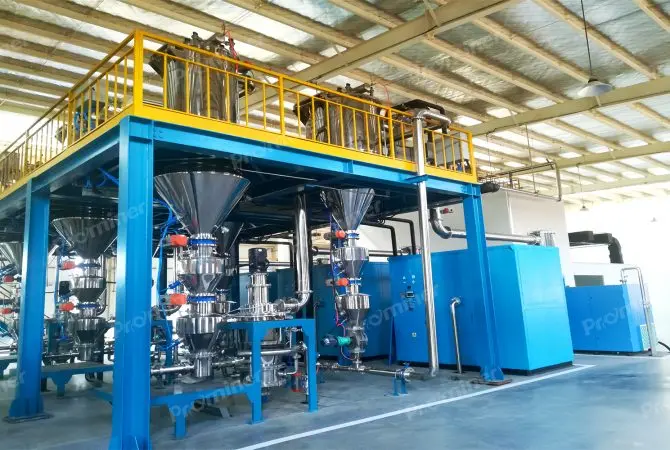
Jet mill is also called fluidized bed jet mill by using multiple nozzles to form sonic speed air flow
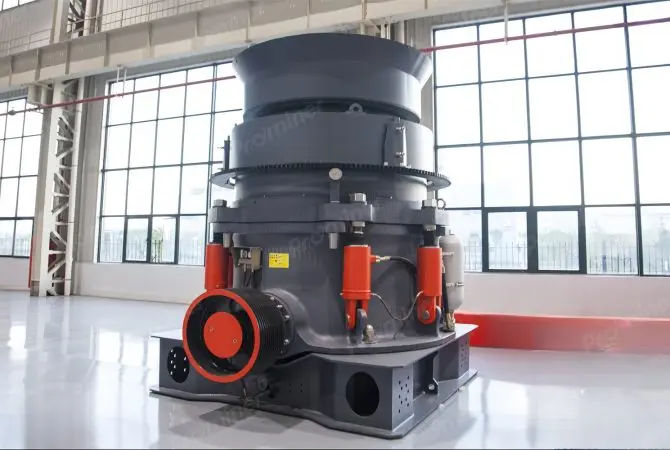
Multi-cylinder hydraulic cone crusher combines crusher speed, eccentricity and cavity profile
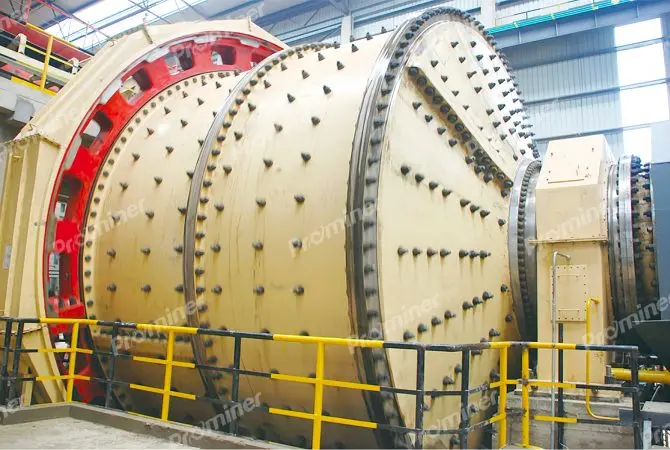
AG/SAG is short for autogenous mill and semi-autogenous mill, it combines with two functions of crushing
To find out more about our products and solutions, please fll out the form below and one of our experts will get back to you shortly
3000 TPD Gold Flotation Project in Shandong Province
2500TPD Lithium Ore Flotation in Sichuan
Fax: (+86) 021-58779592
Address: Room 606, Building D3, Phase II, Chuansha Business Center, 777 Long, Miaochuan Road, Pudong New Area, Shanghai,China
Copyright © 2023. Prominer (Shanghai) Mining Technology Co.,Ltd.